


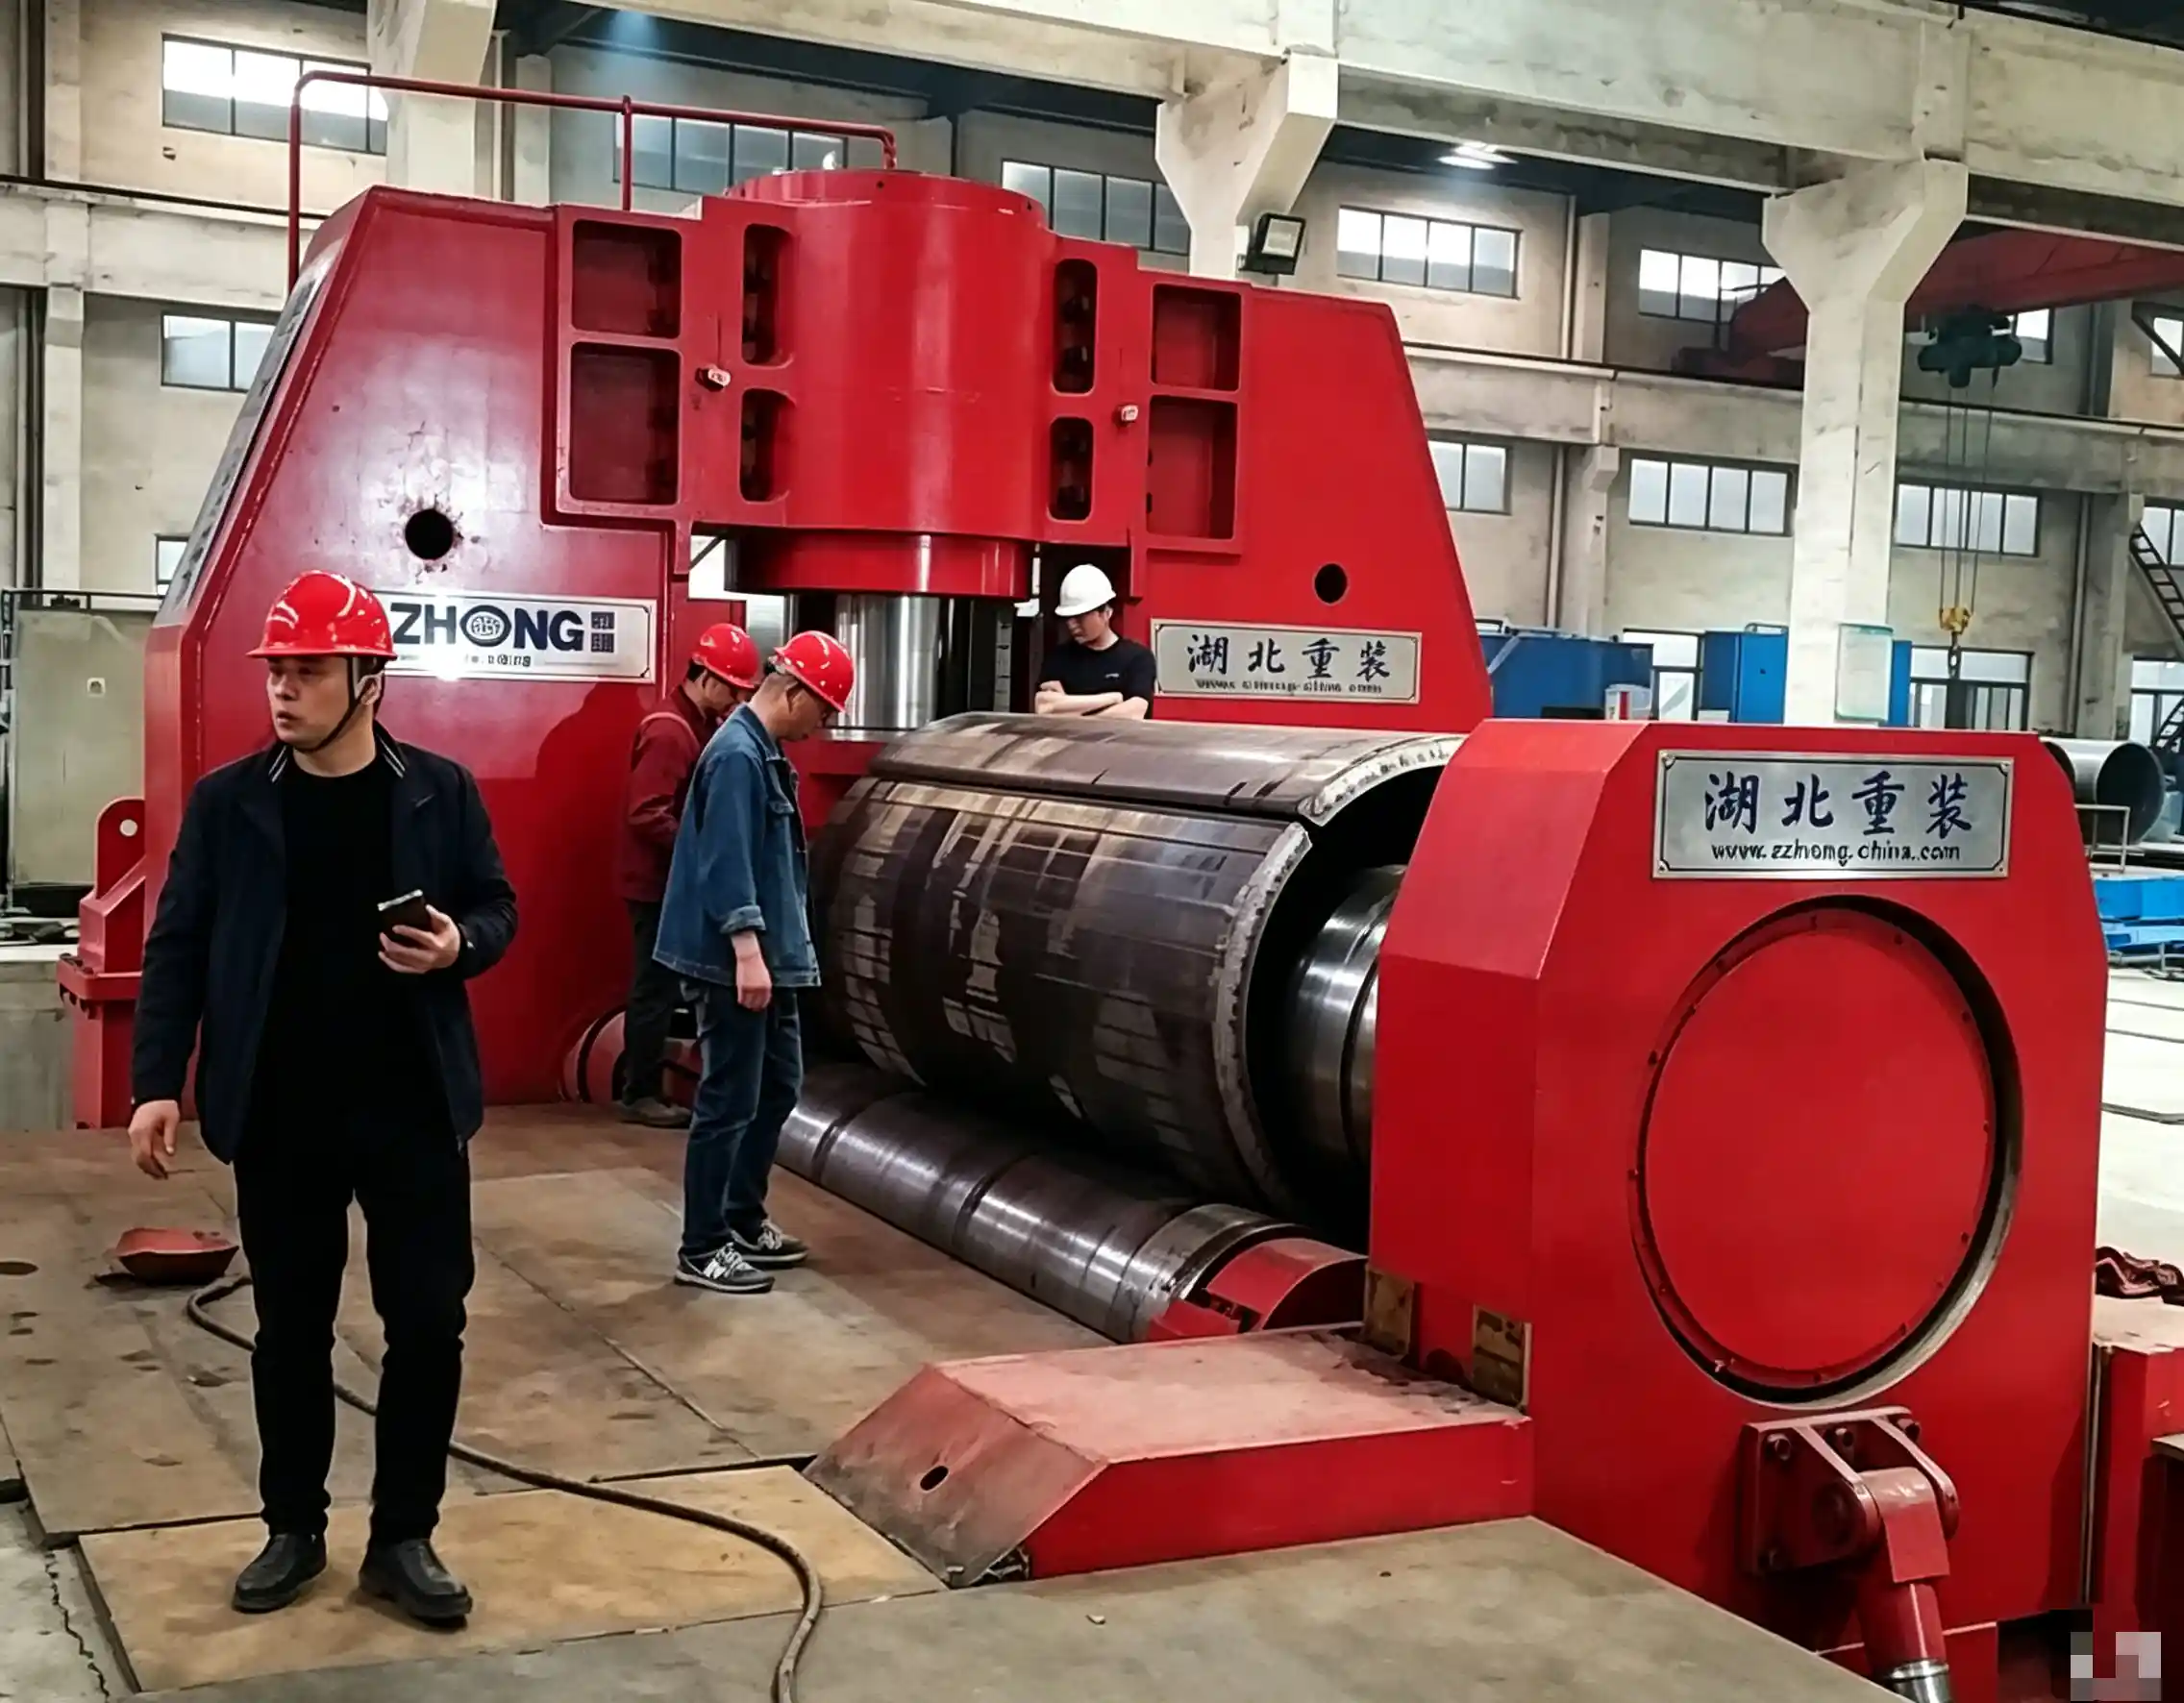
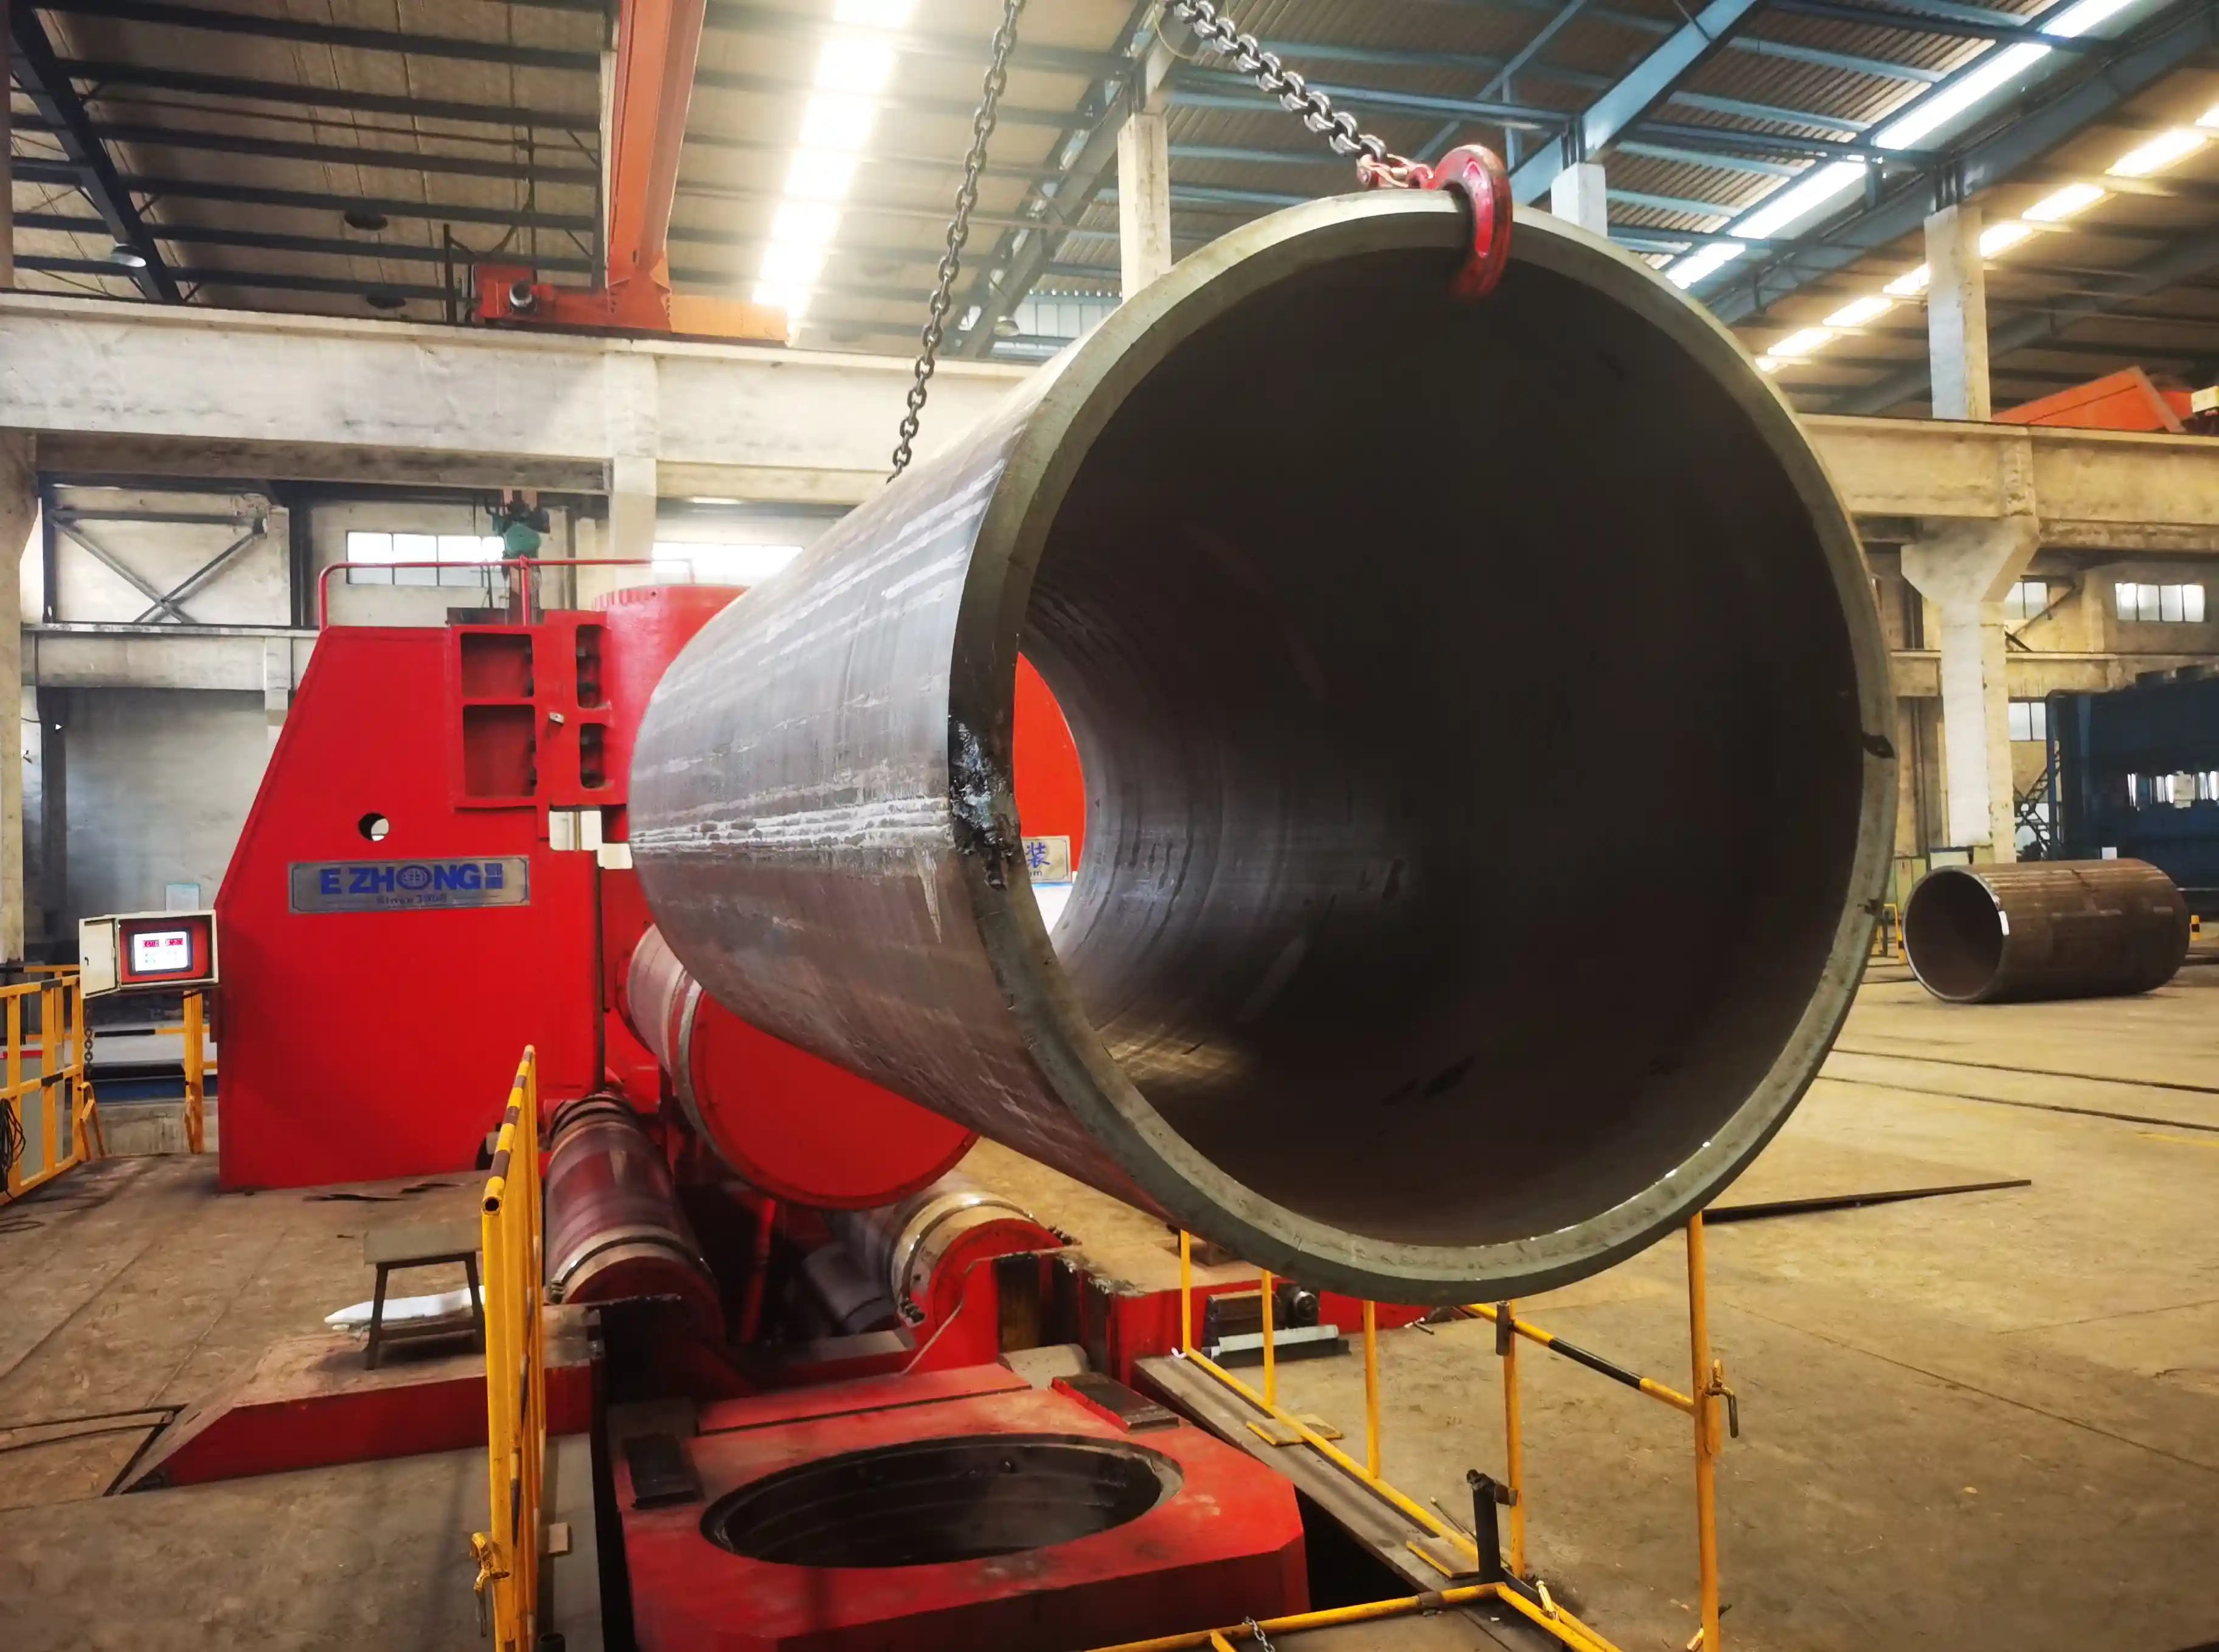
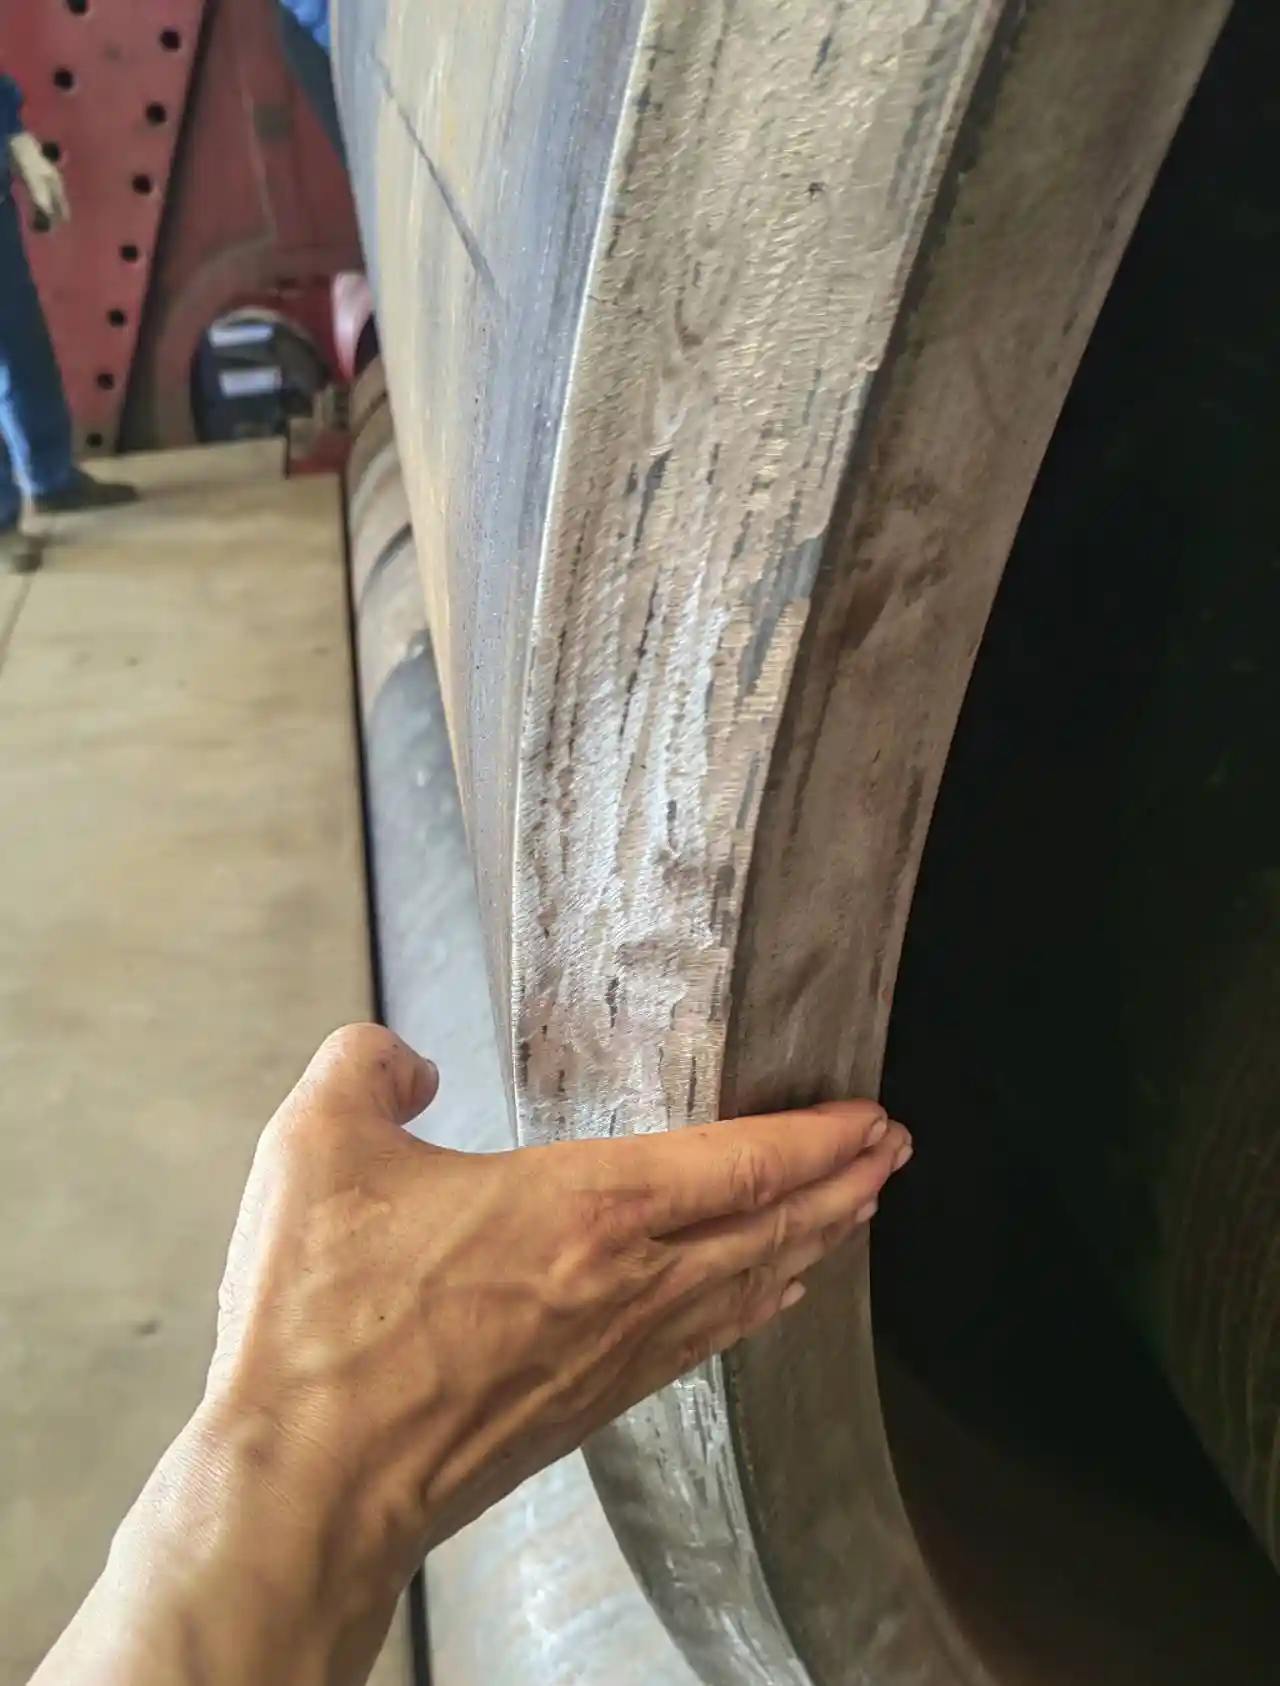
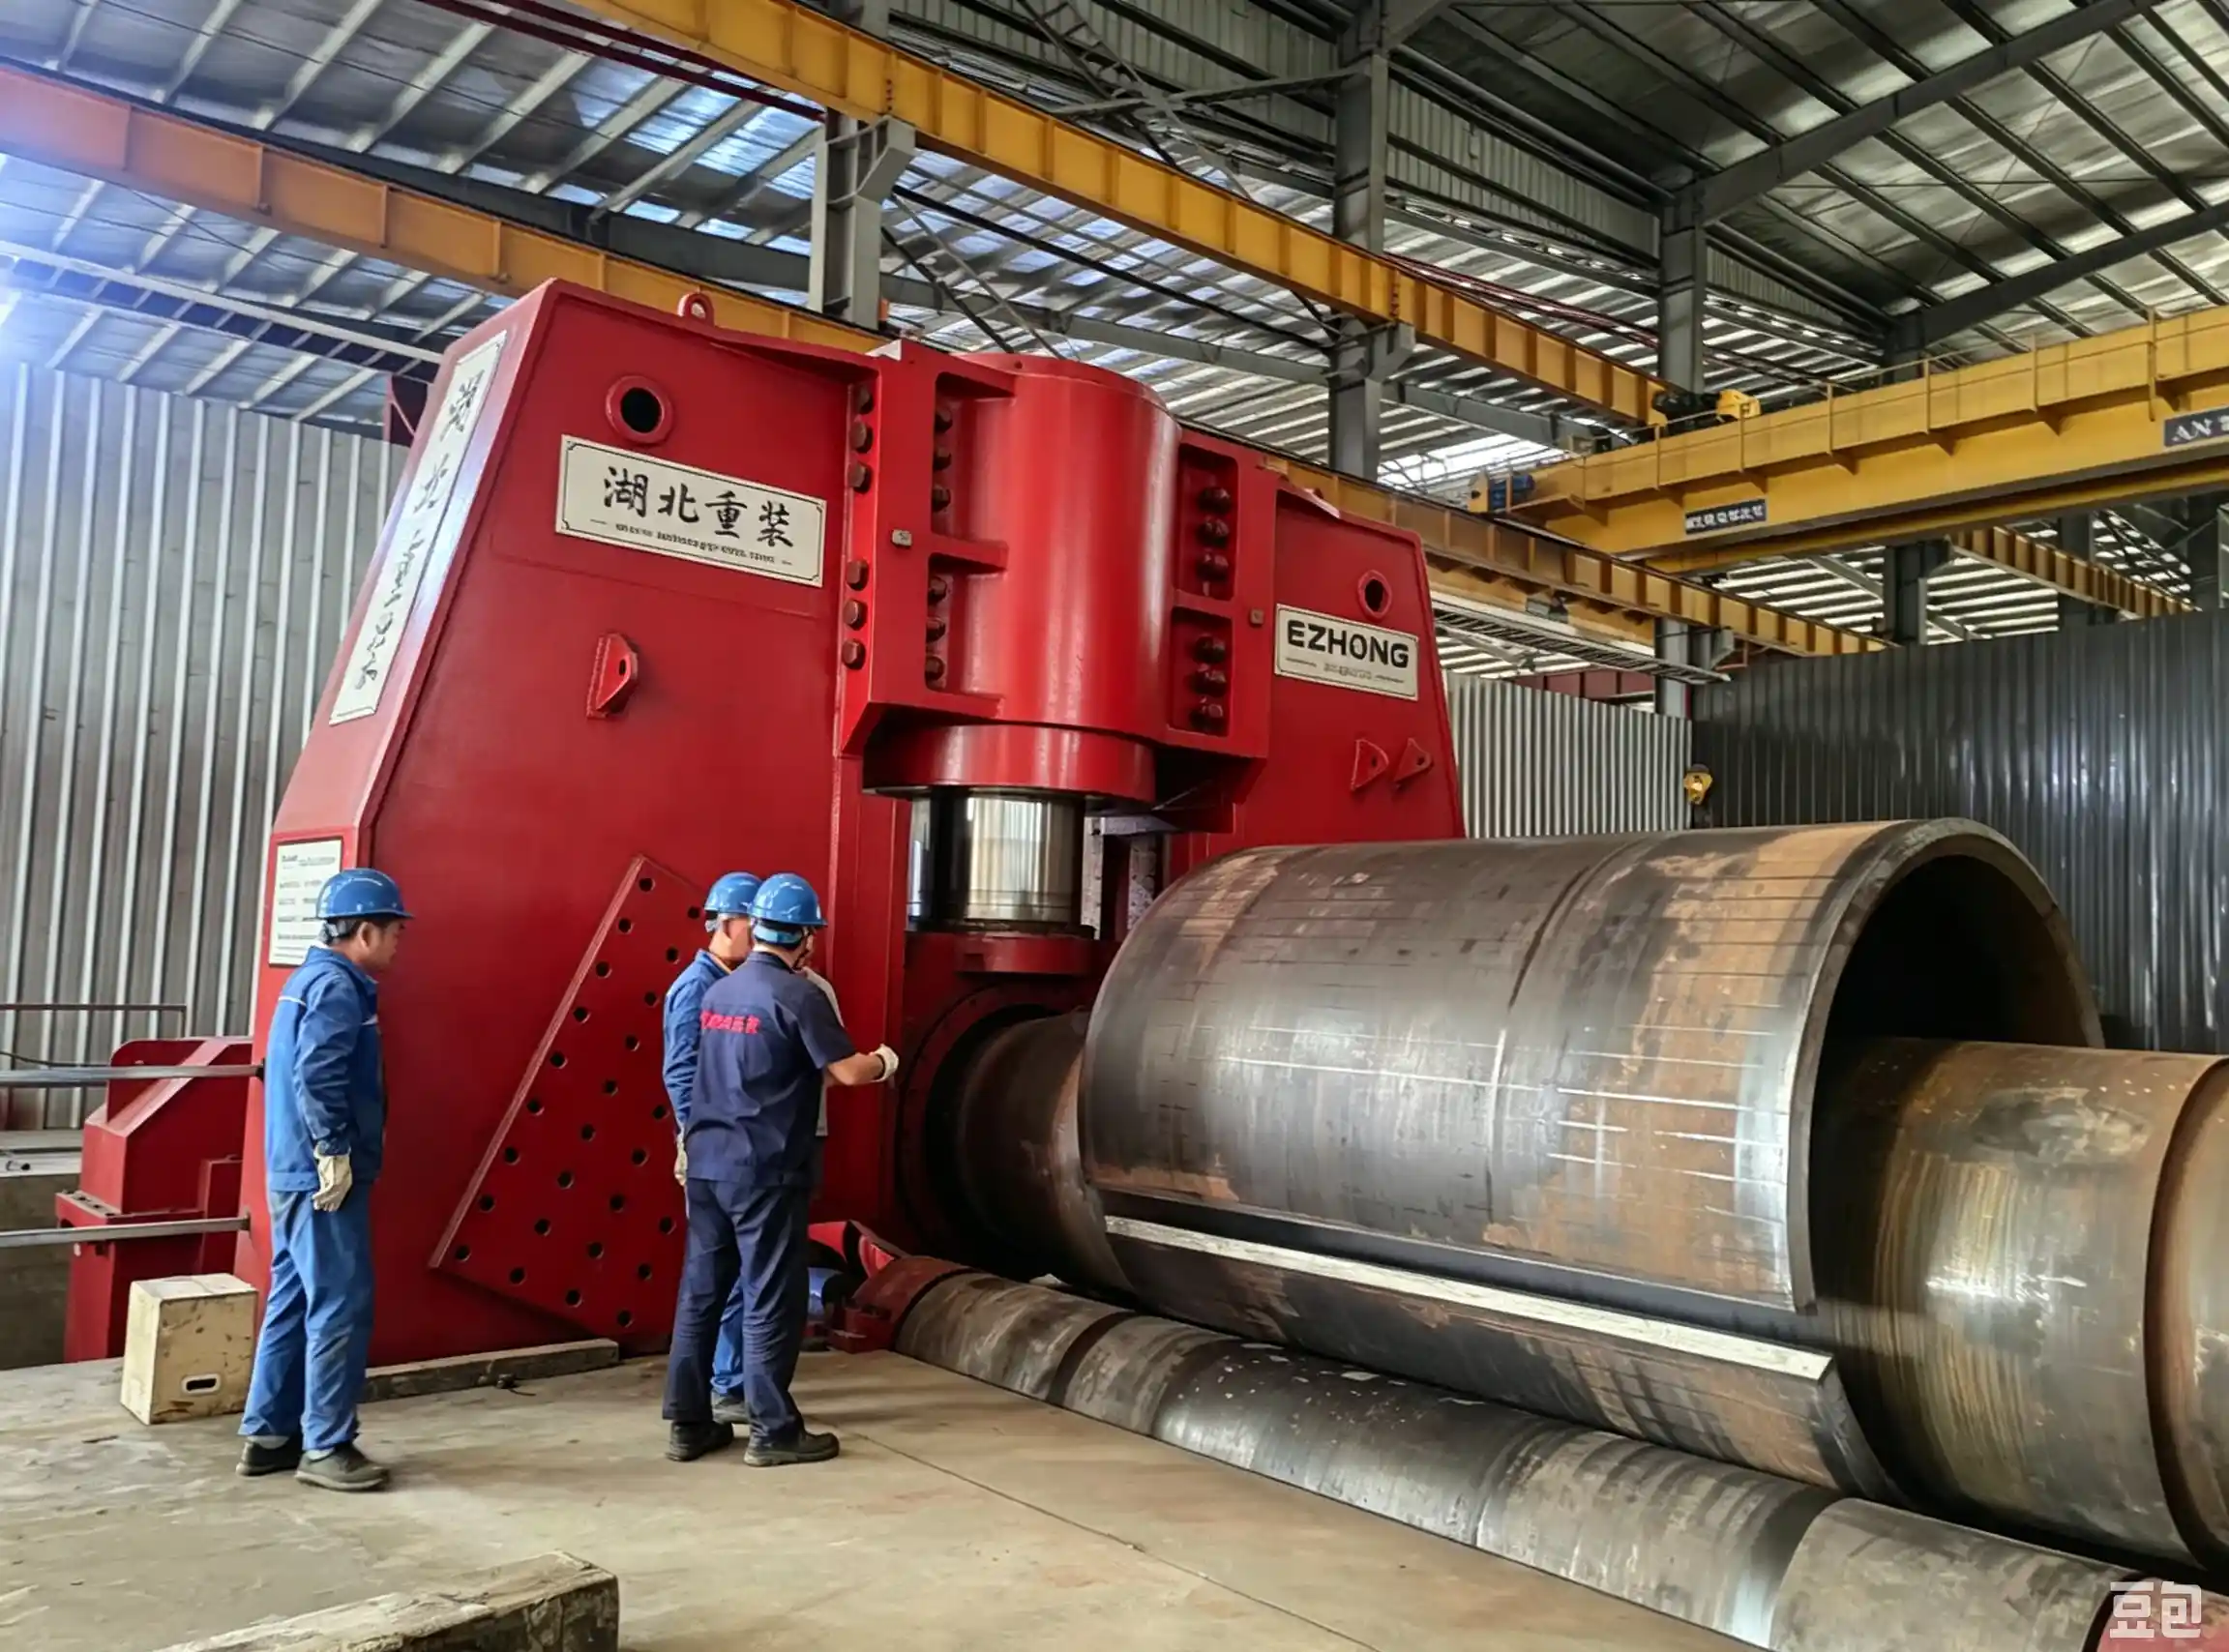
Adjust lower roller spacing in real-time to achieve optimal bending radius for different plate specifications—from thin sheets to heavy-duty thick plates—all on a single machine.
Upper roller features top-mounted main hydraulic cylinder; lower rollers independently driven for asymmetric four-point bending. Eliminates mechanical interference, extends roller life 40% longer.
Computer-controlled vertical positioning with ±0.2mm synchronization accuracy. Real-time LCD display ensures consistent bending quality across the entire plate width.
Controlled lower roller movement enables smooth pre-bending operations. Reduces the minimum bending diameter by 40% compared to fixed-geometry machines.
Hydraulic tilt adjustment of lower rollers (or upper roller when required) with support fixtures enables cone/tapered shell production within the same machine footprint.
During pre-bending operations, steel plates remain horizontally positioned, ensuring superior operator safety and easier measurement of bend plates destined for welding.
Challenges in High-Force Small-Diameter Cylinder Forming
In nuclear power, offshore structures, and heavy-duty pressure vessel manufacturing, thick and high-strength plates often need to be formed into relatively small-diameter cylinders. Conventional three-roll plate bending machines may face significant challenges under these demanding forming conditions.
The machine's defining innovation: each lower roller can move independently horizontally, generating any desired pitch. The upper roller features vertical movement controlled by dedicated hydraulic cylinders.
Precision Metrics:Center Distance Adjustment: <2s | Positioning Accuracy: ±2mm | Synchronization: ±0.2mm across plate width
Unique hydraulic design with smooth unloading at high pressure levels, preventing workpiece bounce and eliminating harmful "water hammer" effects on hydraulic pipelines.
All three working rollers are main drive rollers. Upper roller driven by single hydraulic motor through planetary reducer; lower rollers each driven independently through dedicated planetary reducer systems.
Specialized tilt mechanisms on both upper and lower bearing seats enable tapered shell production.
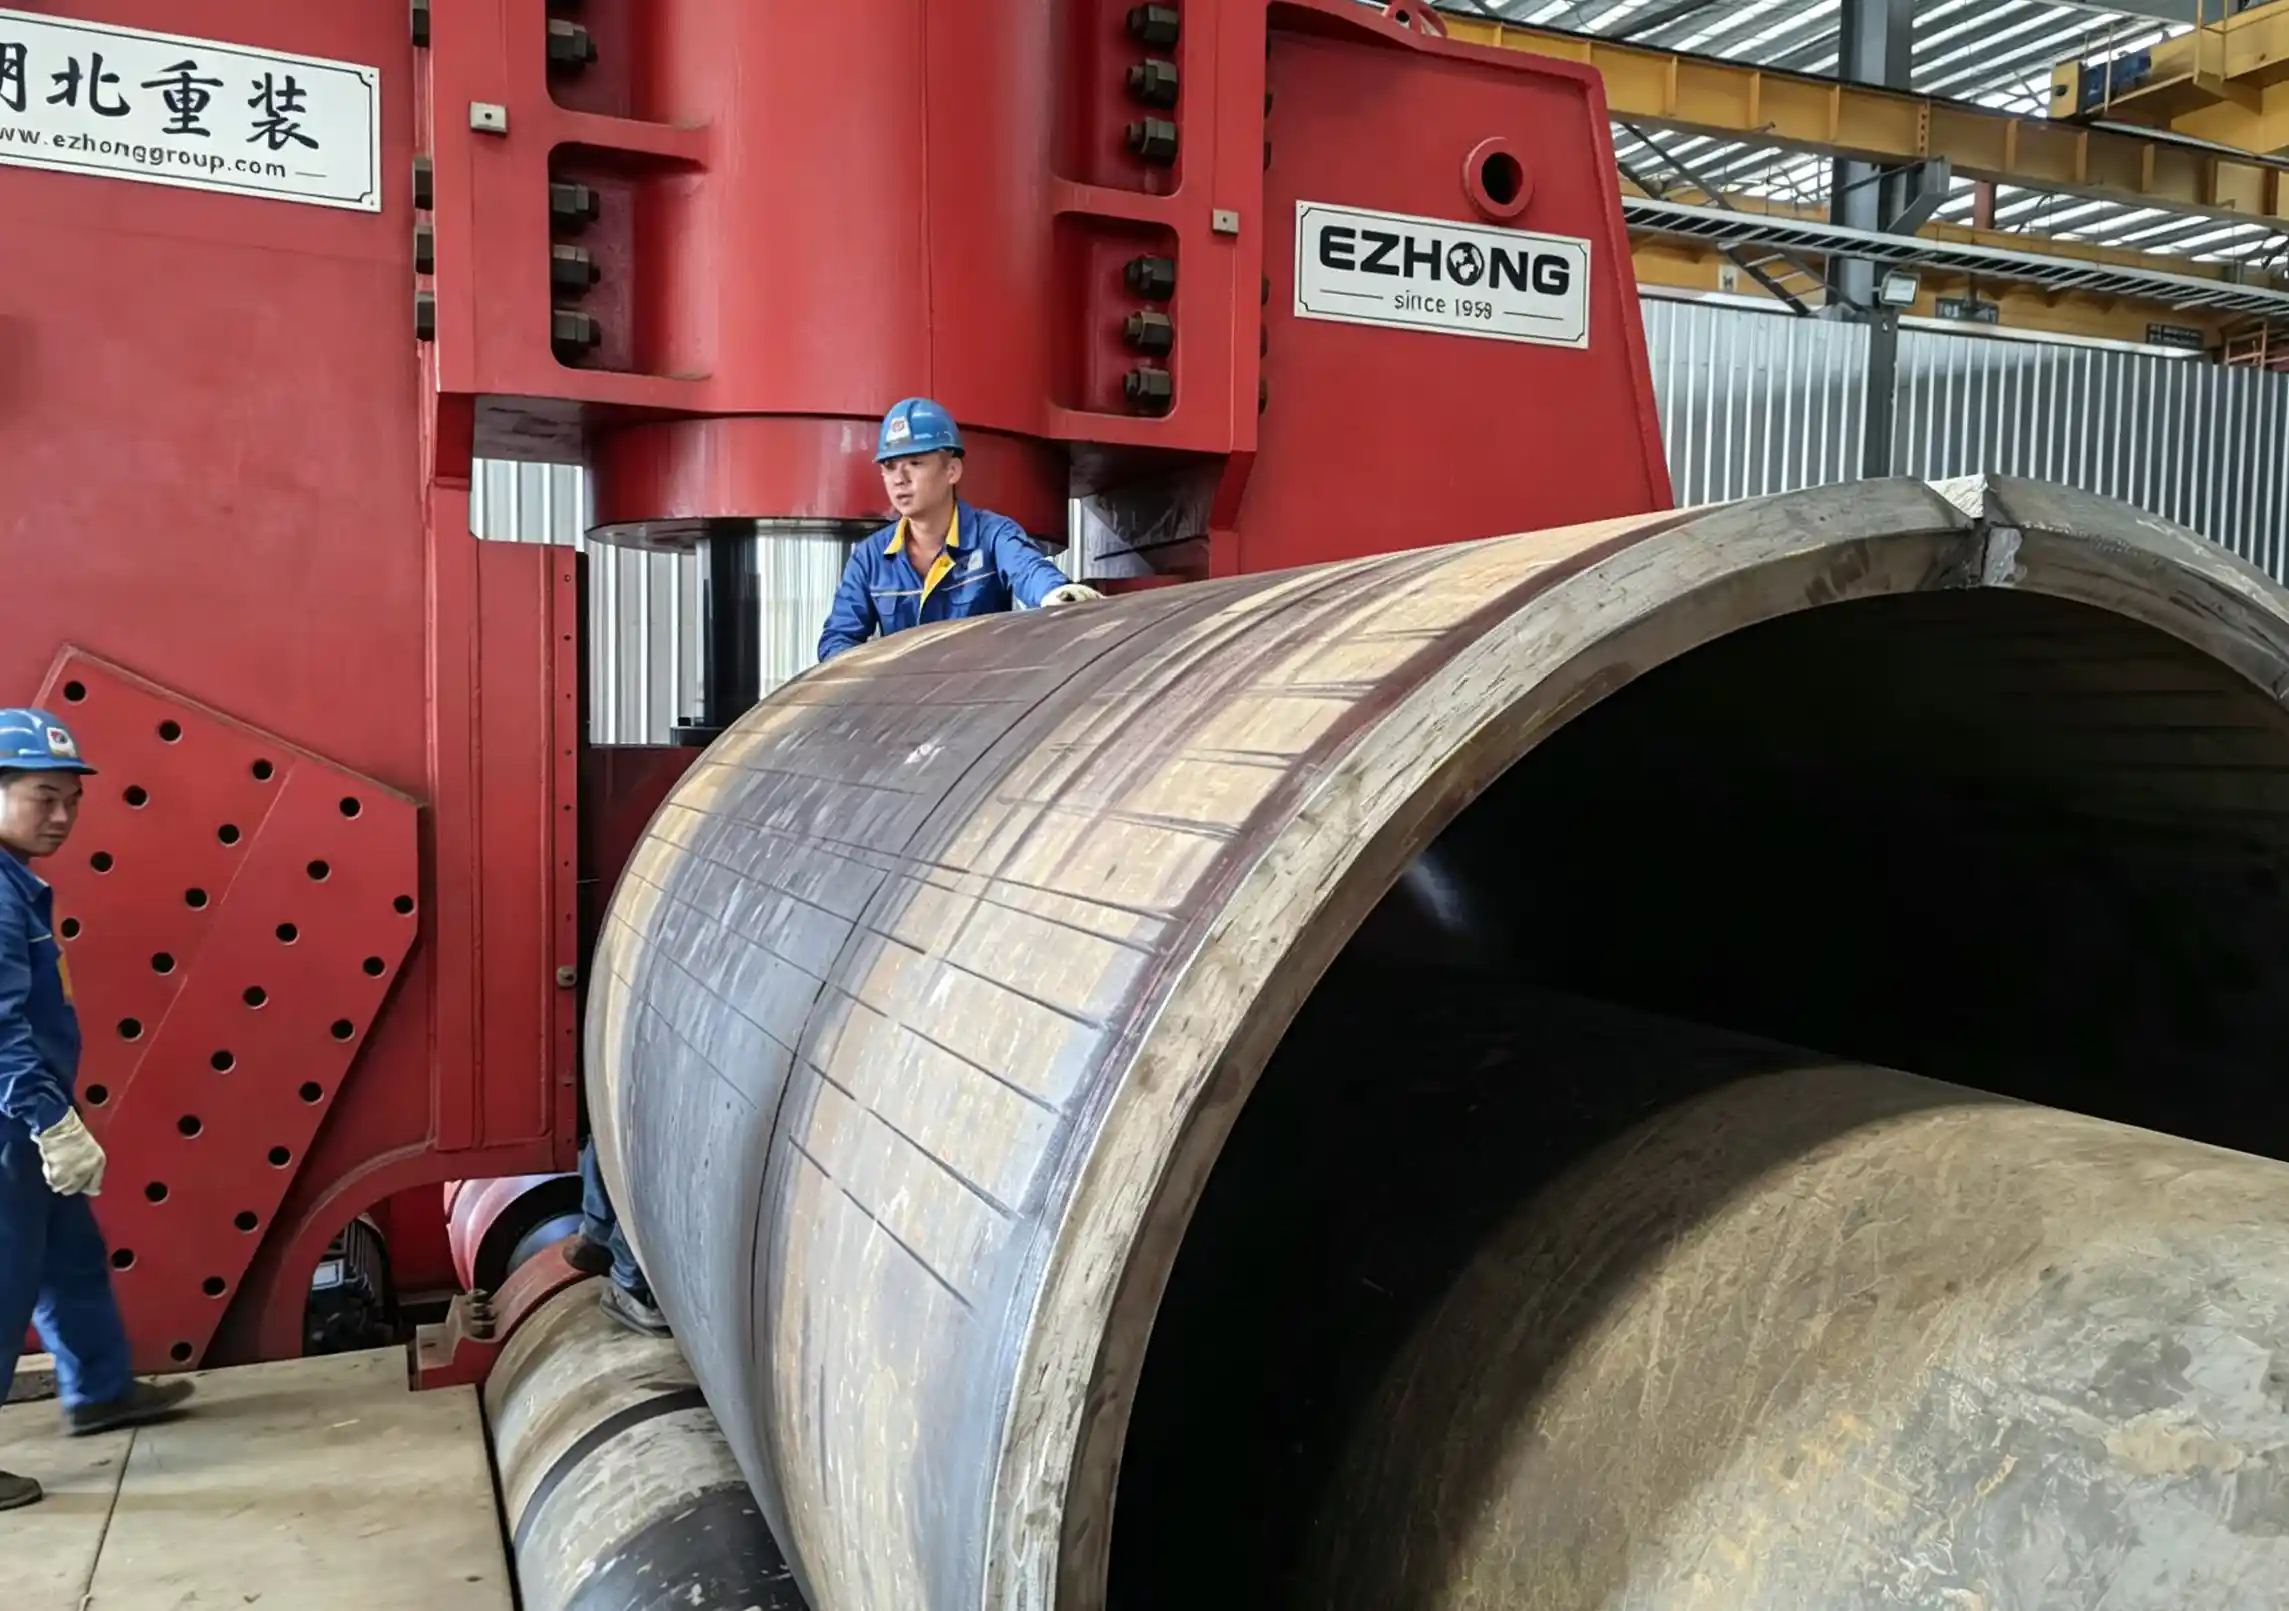
Integrated Siemens PLC + industrial touch screen, equipped with self-balancing algorithm for full automatic rolling.
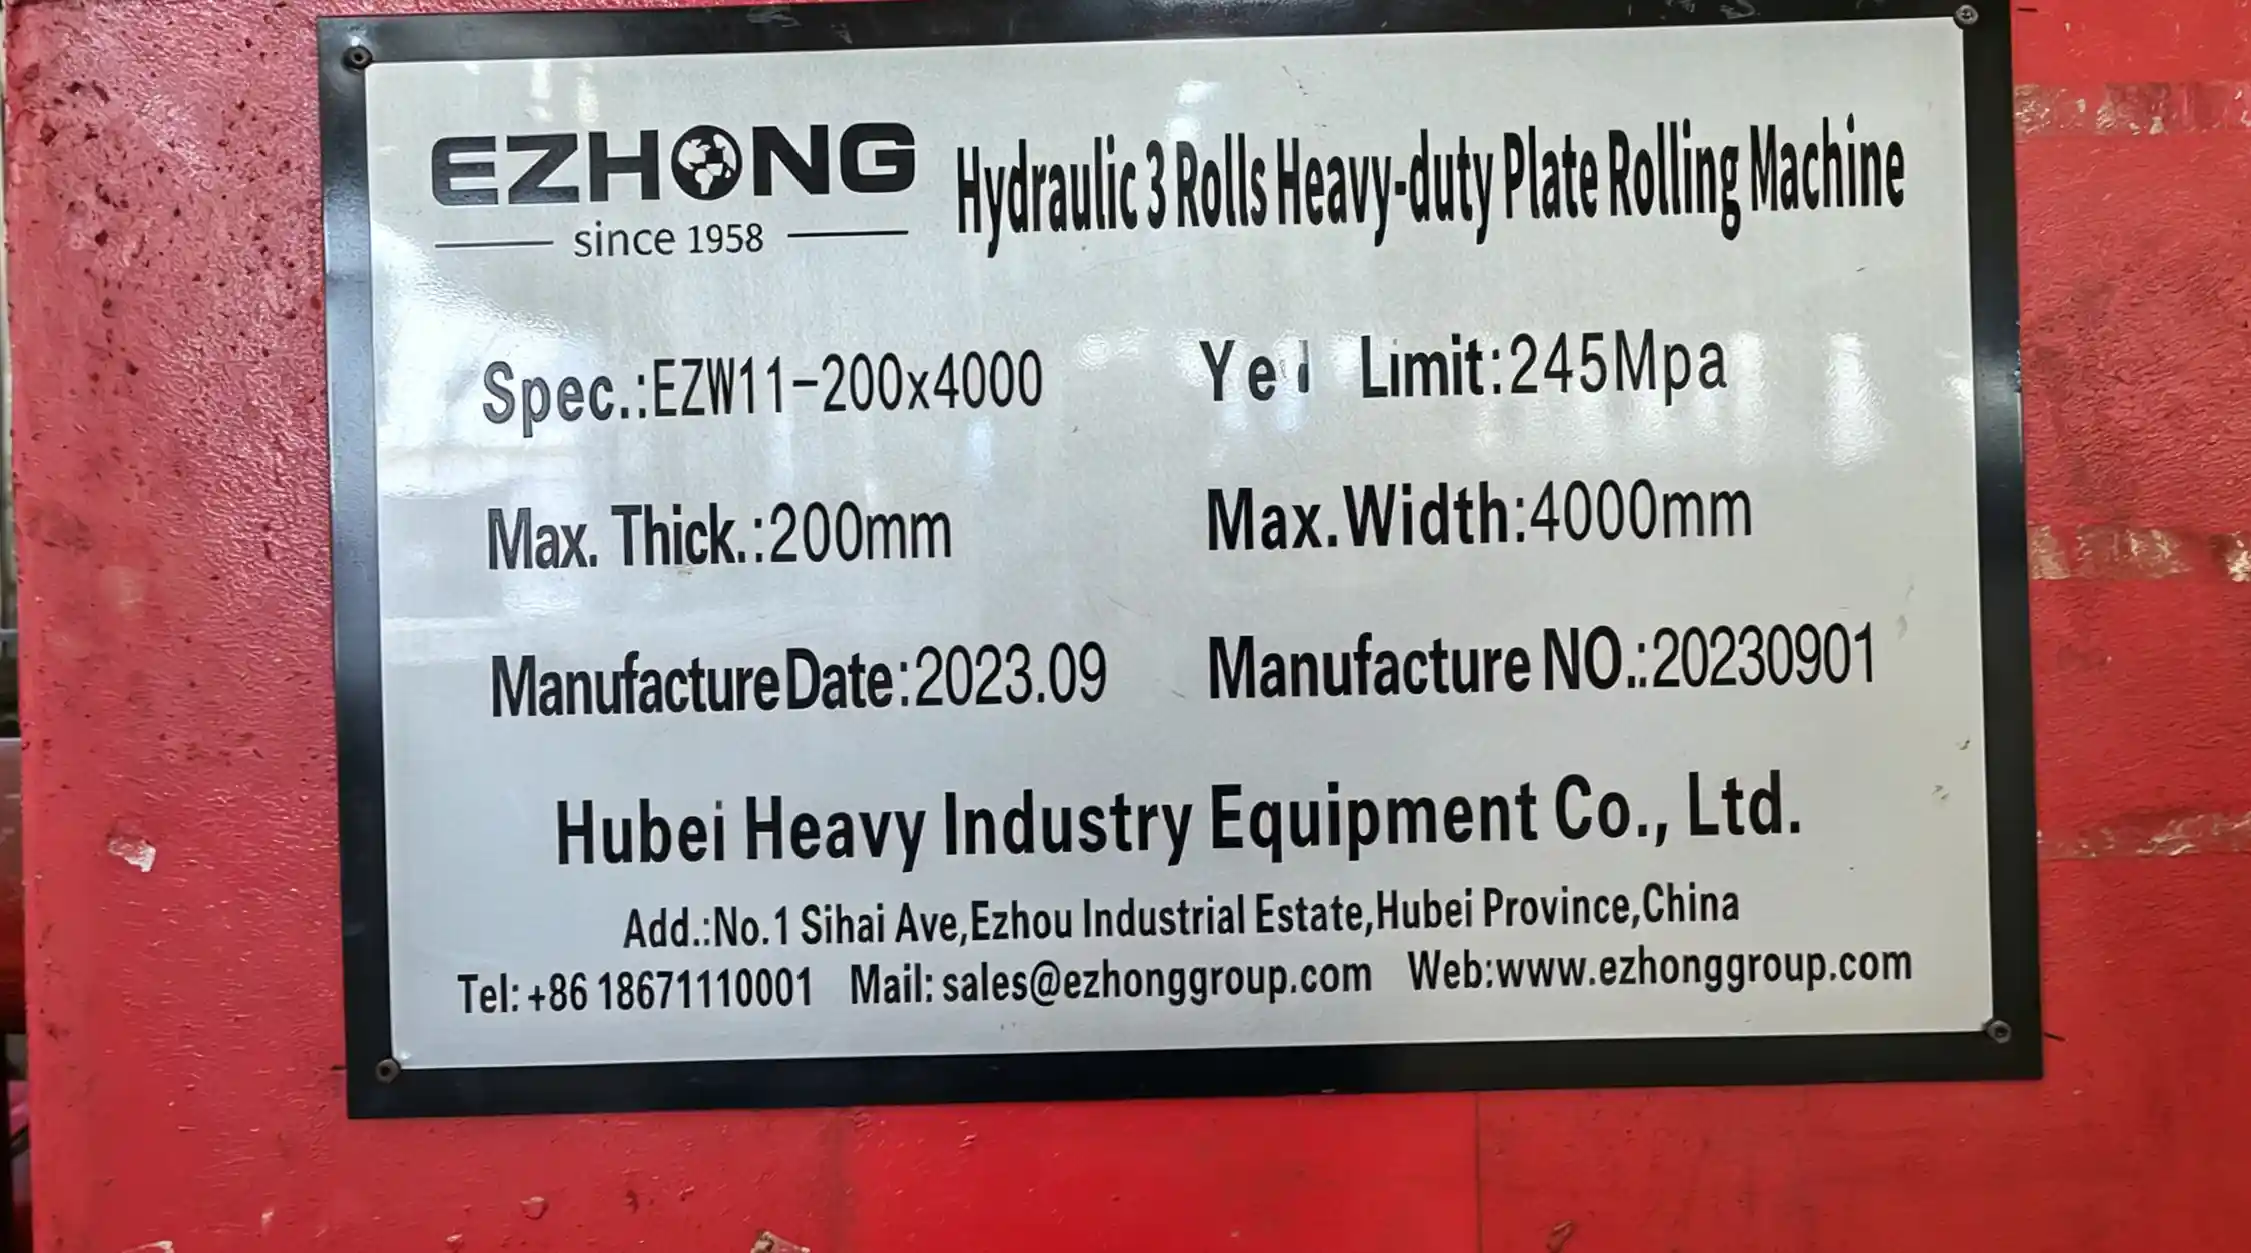
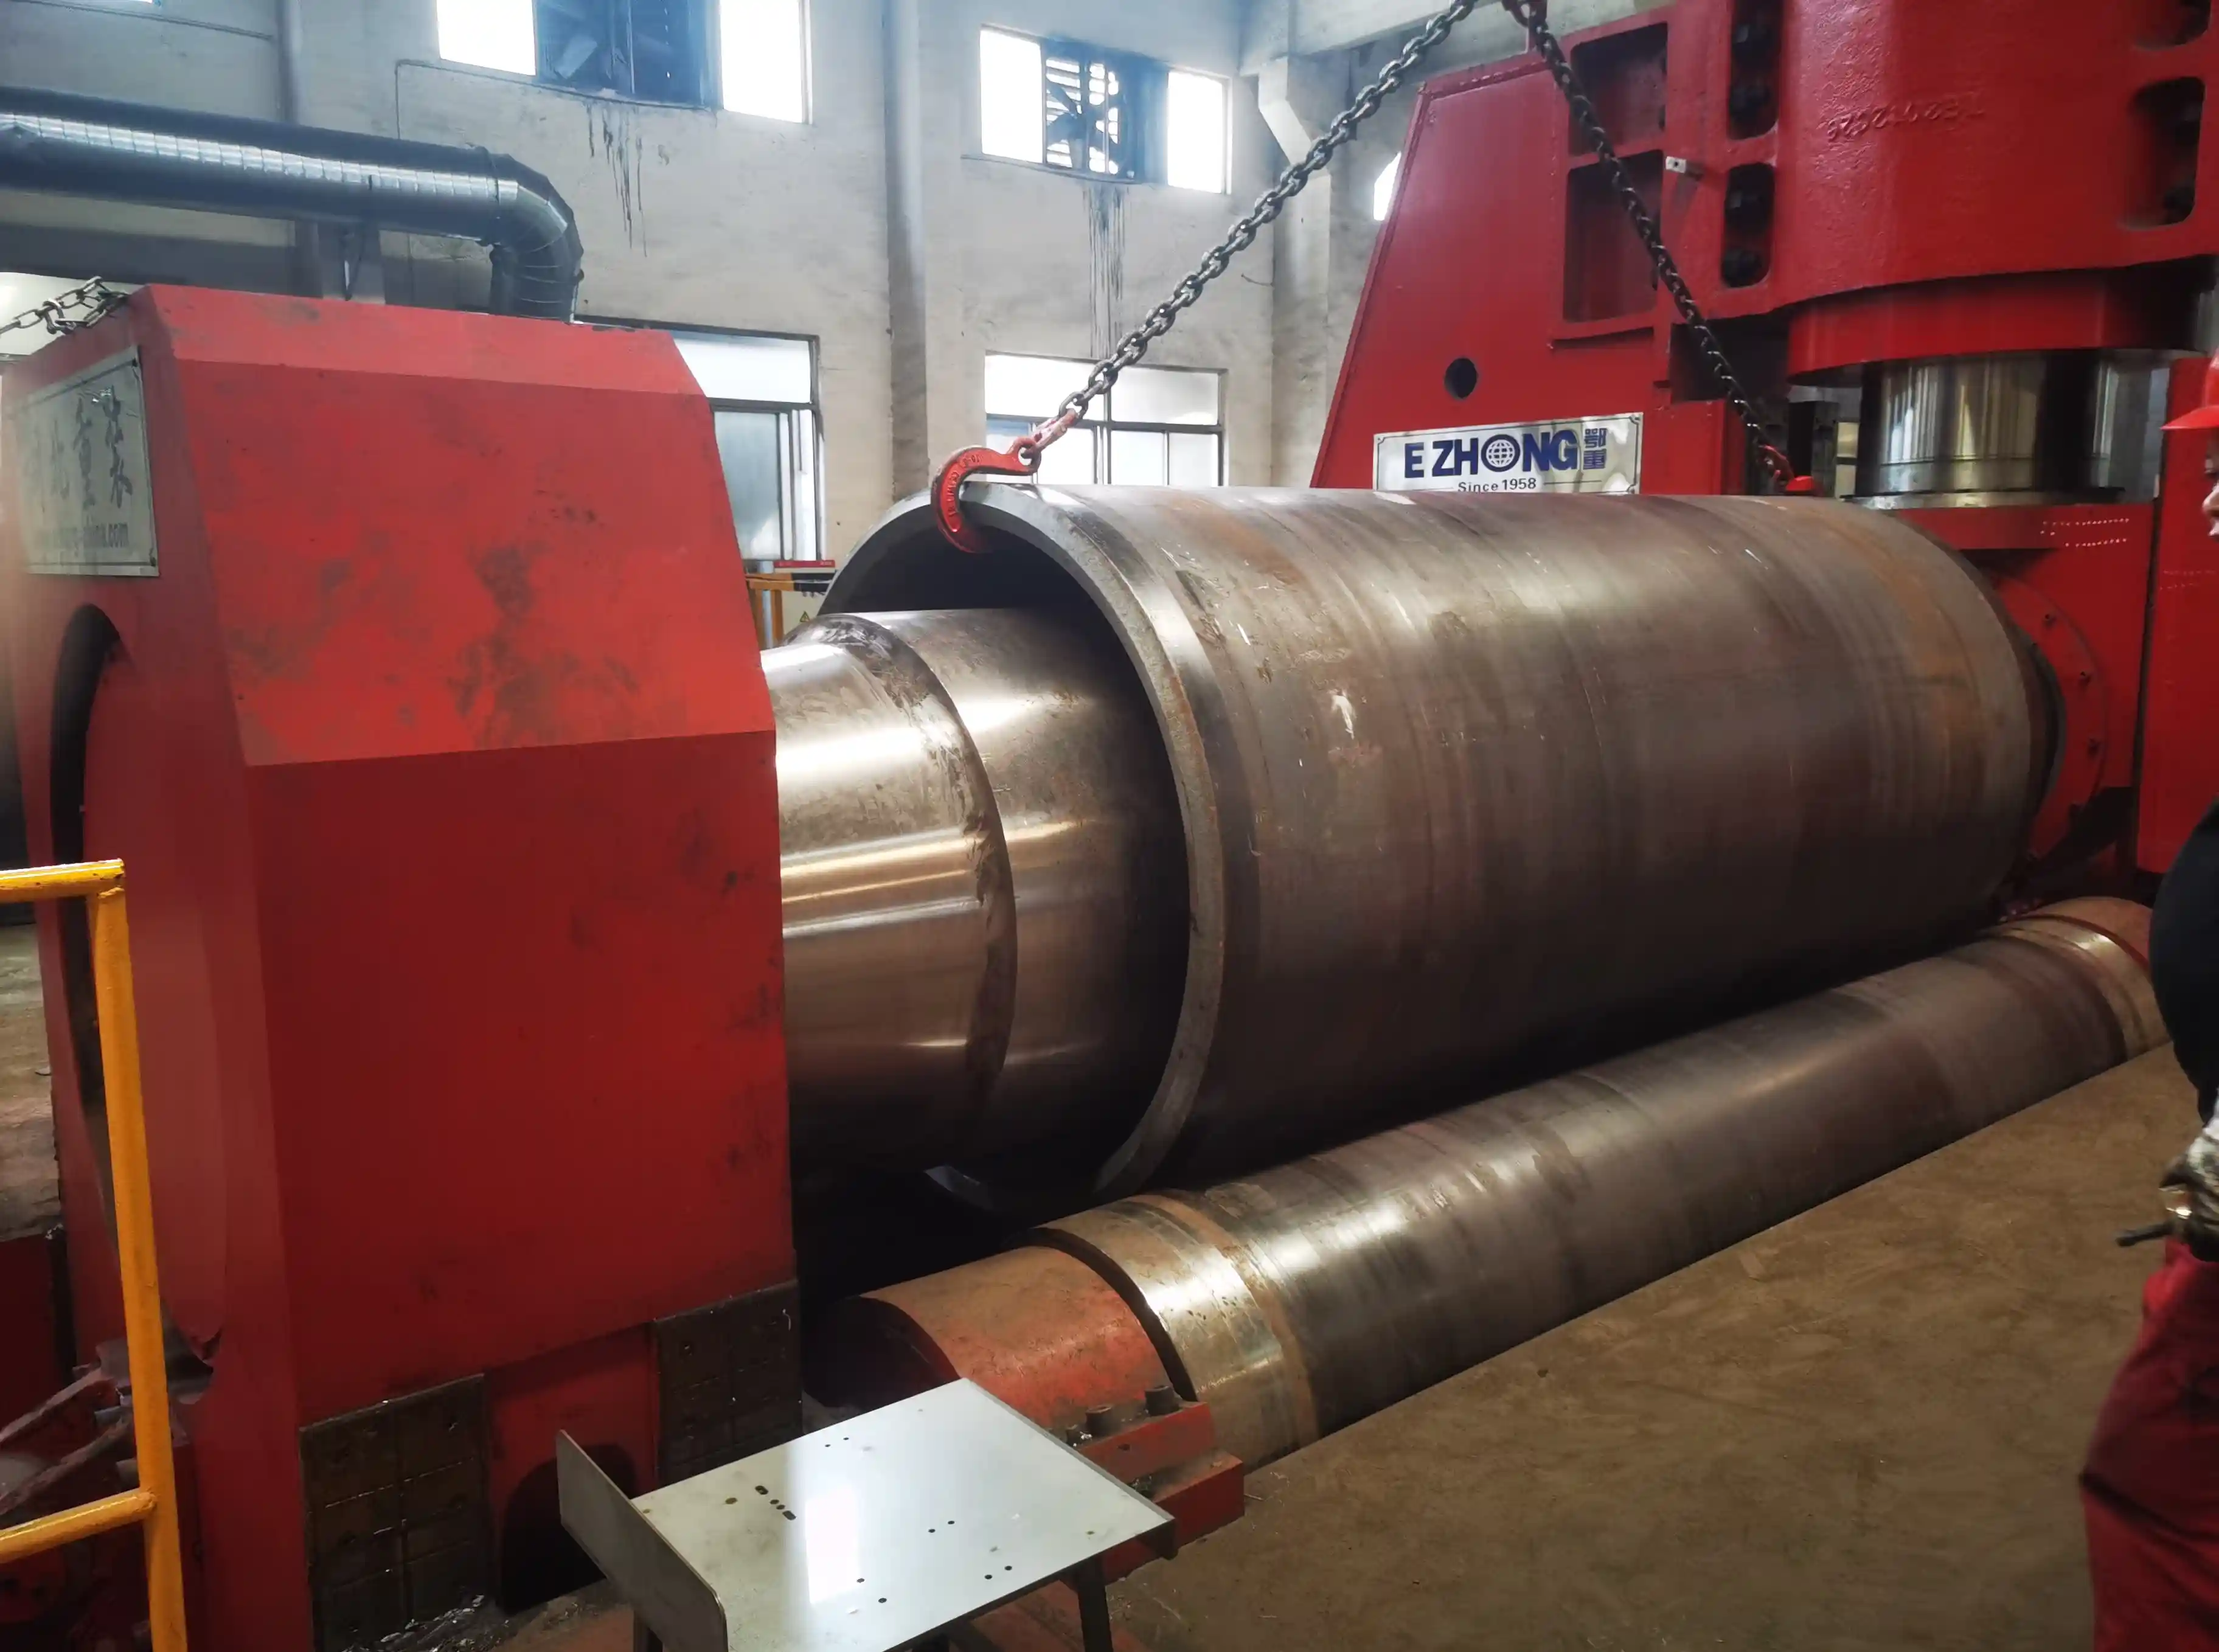
High-strength stress-relieved steel plate, CNC finish, rigid frame without deflection under 8000T load, horizontal accuracy ±0.5mm full length.
42CrMo forged rollers, mirror polished Ra≤0.4μm, hot rolling version withstands 300°C continuous working temperature.
Variable displacement plunger pump, independent proportional valve control, 2500-4500L oil capacity, 10μm precision filtration.
Siemens S7-1200 PLC, 7-inch bilingual touch screen, LVDT high precision position sensor, IEC standard circuit protection.
| Model | Plate Width (mm) | No Pre-Bend (mm) | Pre-Bend (mm) | Main Motor Power (kW) | Rolling Speed (m/min) | Dimensions L×W×H (mm) |
|---|---|---|---|---|---|---|
| EZW11S-35×2000 | 2000 | 35 | 25 | 37.5 | 1.5-5 | 5450×2800×2000 |
| EZW11S-40×2000 | 2000 | 40 | 35 | 48 | 1.5-5 | 6000×2800×2000 |
| EZW11S-50×2000 | 2000 | 50 | 40 | 52 | 1.5-5 | 6100×2800×2200 |
| EZW11S-60×2000 | 2000 | 60 | 50 | 73.5 | 1.5-4 | 6900×3100×2650 |
| EZW11S-65×2000 | 2000 | 65 | 55 | 73.5 | 1.5-4 | 7050×3350×2700 |
| EZW11S-30×3000 | 3000 | 30 | 20 | 37.5 | 1.5-5 | 5950×2800×2000 |
| EZW11S-35×3000 | 3000 | 35 | 25 | 48 | 1.5-5 | 6500×2800×2000 |
| EZW11S-45×3000 | 3000 | 45 | 30 | 52 | 1.5-5 | 6600×2800×2200 |
| EZW11S-50×3000 | 3000 | 50 | 35 | 73.5 | 1.5-4 | 7400×3100×2650 |
| EZW11S-60×3000 | 3000 | 60 | 40 | 73.5 | 1.5-4 | 7550×3350×2700 |
| EZW11X-70×3200 | 3200 | 70 | 60 | 60+24.1 | 4.00 | 7980×3320×3680 |
| EZW11X-100×3200 | 3200 | 100 | 90 | 104+32.2 | 4.00 | 8600×4160×4490 |
| EZW11X-150×3200 | 3200 | 150 | 135 | 150+84.2 | 3.20 | 10430×4970×5850 |
| EZW11X-200×3200 | 3200 | 200 | 180 | 220+93.7 | 3.12 | 12100×6160×7460 |
Answer a few quick questions to help us recommend the most suitable plate bending machine for your application.
ASTM A516 Gr.70 / 16MnDR, thickness 50-200mm, roundness tolerance ±2mm.
API X80/X120 pipe, thickness 30-150mm, ovality control ±1.5%.
Q345/S355 structural steel, thickness 20-100mm, flat edge tolerance ≤3mm/1000mm.
Q235/A36 storage tank, thickness 8-60mm, high pre-bend accuracy for assembly.
SA516/15Mo3 boiler drum, thickness 40-120mm, precise circularity for flange matching.
304/316L stainless steel cone, 15°~45° adjustable angle, smooth transition surface.
Challenge:Frequent mold changeover caused production bottleneck.
Solution:EZW11S-100×3000 VCD CNC model.
Result:+42% output, scrap rate 15%→3%, payback 14 months.
Challenge:X80 thick plate springback caused diameter out of tolerance.
Solution:EZW11X-150×3200 hydraulic pre-discharge system.
Result:Roundness ±1.2mm, save €180,000 outsourcing cost yearly.
Challenge:Tank shell pre-bend inconsistency led to welding distortion.
Solution:EZW11S-60×3000 horizontal pre-bend CNC correction.
Result:Assembly time -35%, annual capacity 500→650 units.
Challenge:Multi-angle cone shell frequent mechanical adjustment.
Solution:EZW11X-200×3200 automatic cone tilt system.
Result:Setup time 2h→8min, machine utilization 68%→92%.
Minimum diameter varies by model. Entry-level EZW11S-35×2000 achieves 1.5m diameter; heavy-duty EZW11X-200×3200 reaches down to 0.8m. The variable center distance allows 40% reduction versus fixed-geometry machines.
Three independent LVDT position transducers measure upper and lower roller height in real-time. The Siemens PLC compares actual vs. target positions 50 times/second and adjusts hydraulic valve solenoids within ±2mm, maintaining ±0.2mm flatness.
Yes. Standard configuration is for cold rolling (up to 50°C ambient). Hot rolling variant available with 42CrMo rollers rated to 300°C and enhanced oil cooling. Consult engineering for specific hot-roll requirements.
24 months from shipment on parts and labor. Covers manufacturing defects. Consumables (seals, bearings) and routine wear parts excluded. Extended warranty available (36-60 months) at additional cost.
Yes. Optional IoT upgrade adds cloud connectivity. Real-time pressure, temperature, cycle data streamed to EZHONG service portal. Predictive alerts issued 2-4 weeks before component failures (±accuracy 85%).
| Accessory | Lead Time | Function | Value Proposition |
|---|---|---|---|
| Vertical Top Support System | 6 weeks | Support large-diameter coils up to 16m | 150-ton lift capacity, auto tilt with cone angle |
| Lateral Side Support Fixture | 4 weeks | Prevent wide plate lateral drift | Hydraulic automatic correction, match thin sheet processing |
| Automatic Plate Feeding System | 8 weeks | Motorized feeding & positioning | 60% labor saving, positioning tolerance <5mm |
| Hot Rolling Configuration | 10 weeks | 300°C high temperature rolling | Enhanced cooling system, high temperature resistant roller |
| Remote Monitoring & Diagnostics | 6 weeks | Cloud real-time machine data tracking | Predictive maintenance, reduce unplanned downtime 80% |