


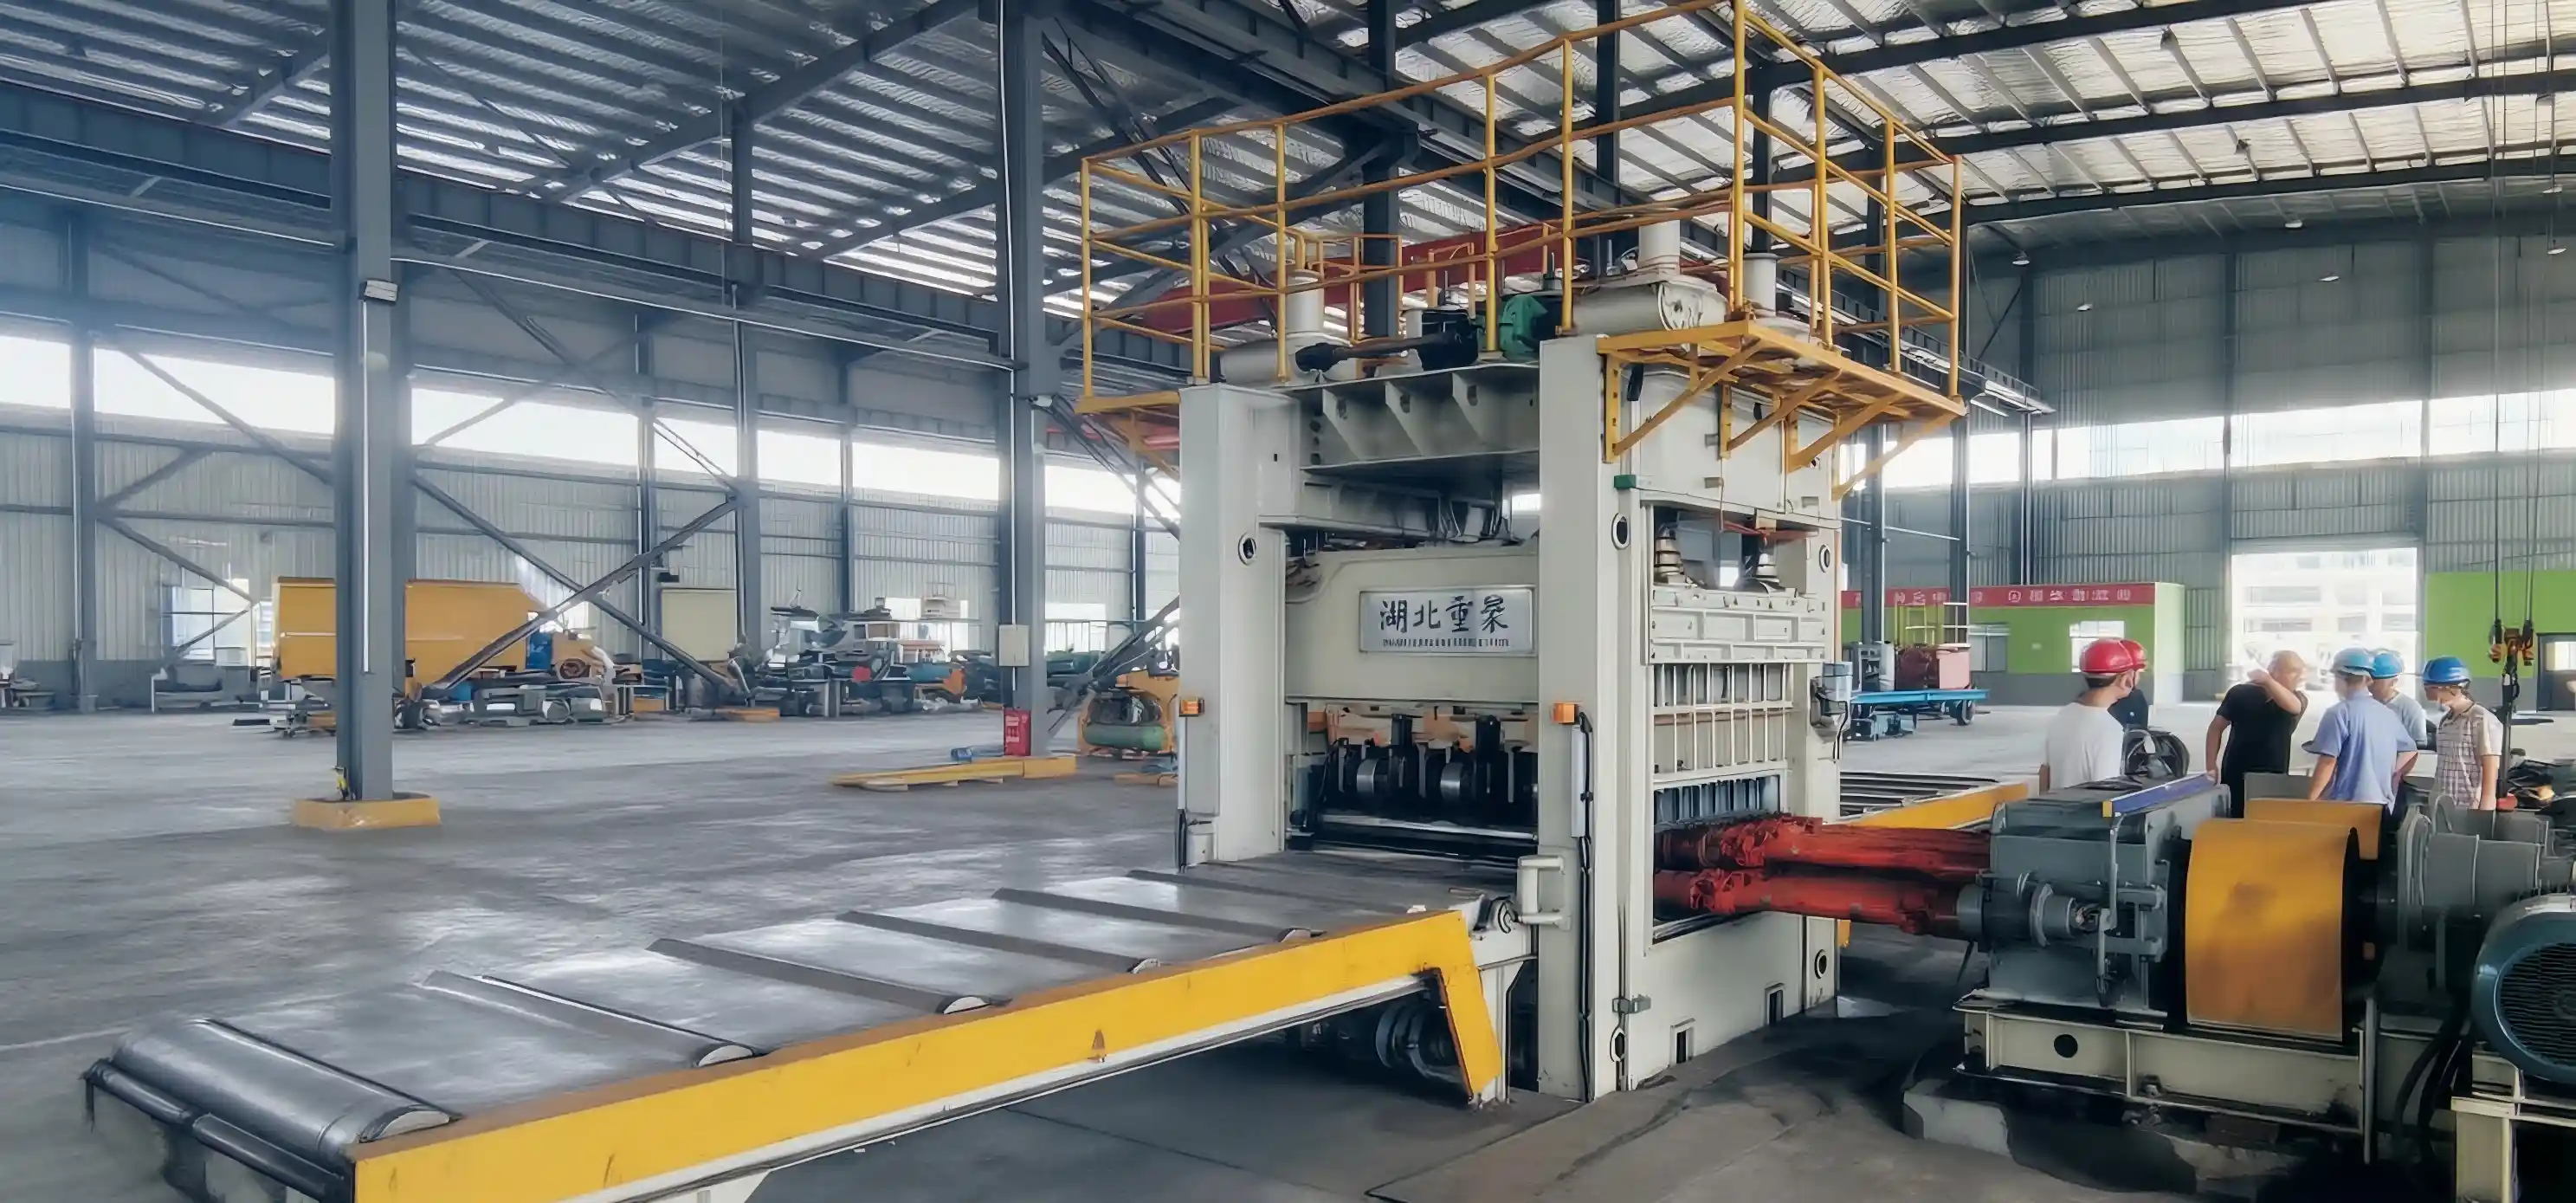
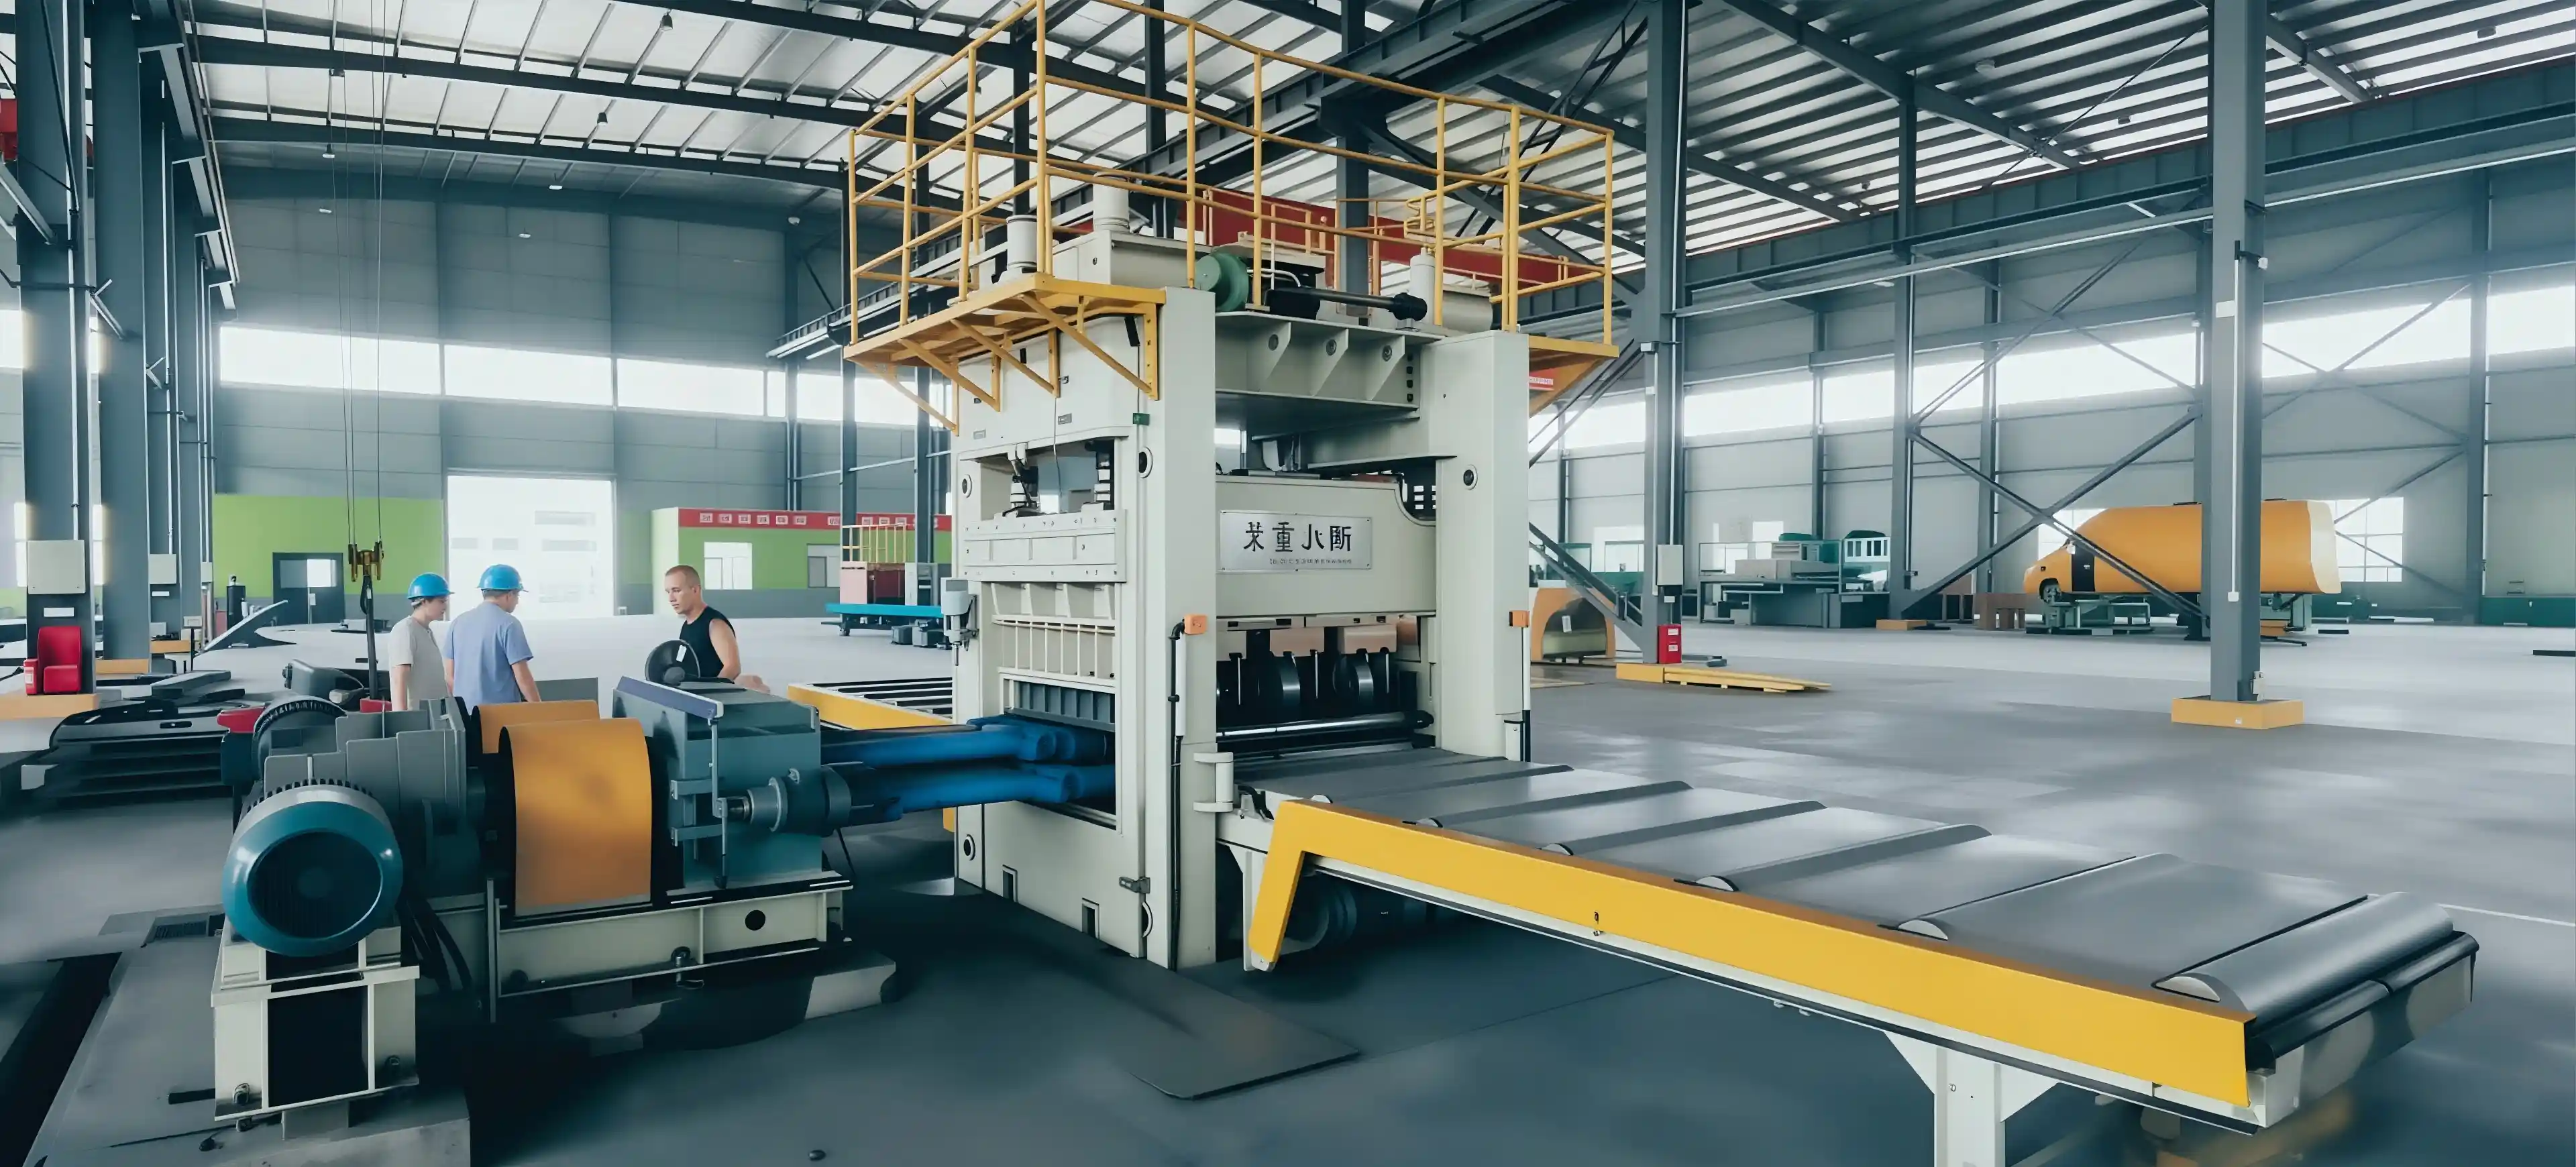
Designed for 3-20mm thickness where precision paramount. 15-roller full primary drive system provides superior distributed force. Achieves ±0.5mm/m² flatness unattainable by traditional equipment. Ideal for applications requiring near-perfect geometry post-leveling.
Both upper and lower work rollers actively driven by independent motors. Zero passive rollers = no slippage, superior surface finish. Each motor delivers 30-45 kW continuous power. Synchronization via proportional valve maintains<±2% torque variance.
Maximum precision configuration: 8 upper rollers + 7 lower rollers in alternating pattern. Reduces individual roller bending moment 60%, extends bearing life 3-4×. Optimal for thin-plate applications where precision, not throughput, is priority.
Four independent pressure transducers monitor inlet/outlet pressures continuously. PLC adjusts proportional valve position<100ms response time. Maintains constant pressure ±3 bar throughout rolling cycle. Achieves precision repeatability ±0.3mm across 100+ consecutive pieces.
4-row backup roller system with each support individually adjustable via wedge mechanism (±0.5mm per position). Eliminates beam deflection entirely. Maintains flatness tolerance independent of plate width or material variance.
System learns pressure curves per material batch. First piece rolled with operator-confirmed settings; system stores parameters. Subsequent pieces processed automatically with ML-based pressure optimization. Reduces operator training time 70%.
All 15 working rollers (8 upper + 7 lower) actively driven. No passive contact rollers. Each roller controlled independently via dedicated motor + proportional valve. Eliminates torque ripple, slip, surface vibration.
Four pressure transducers (inlet, outlet, upper, lower) send real-time signals to PLC. System continuously adjusts proportional valve spool position maintaining target pressure ±3 bar. Achieves precision repeatability ±0.3mm across full production run.
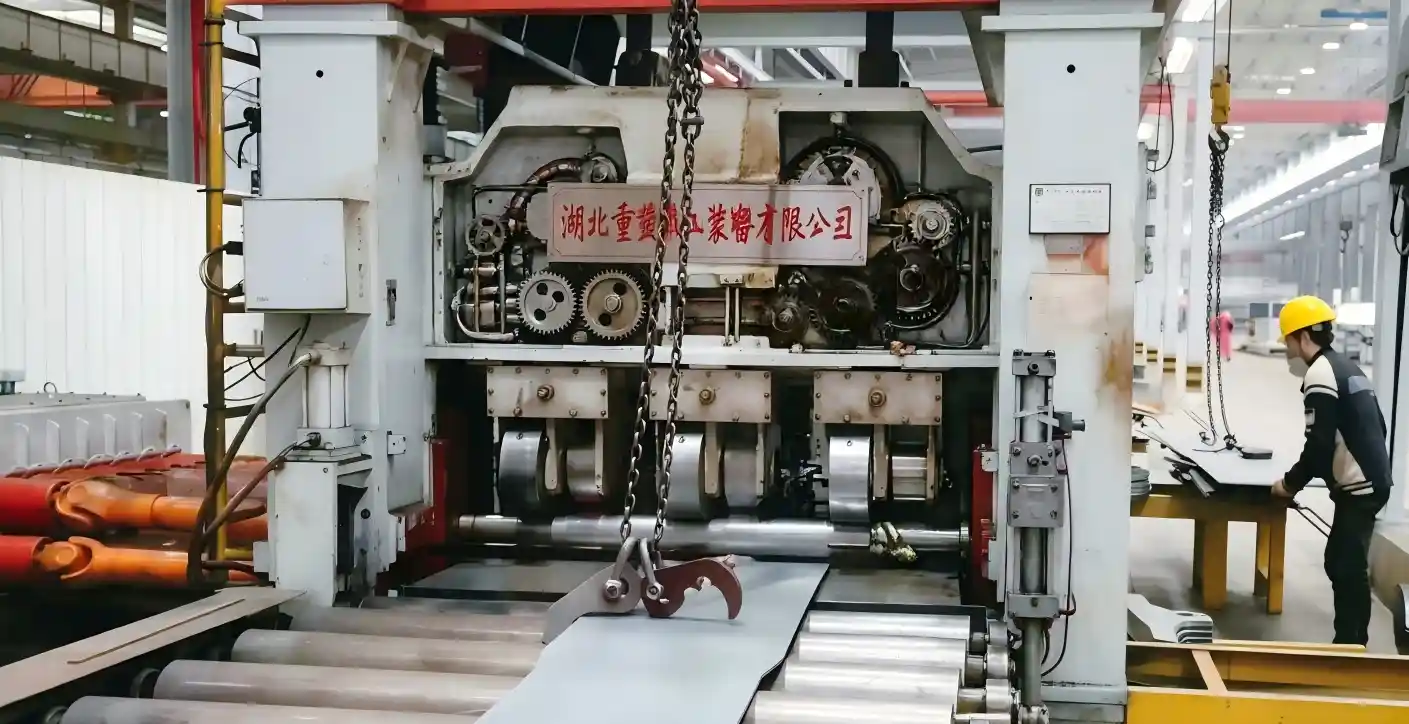
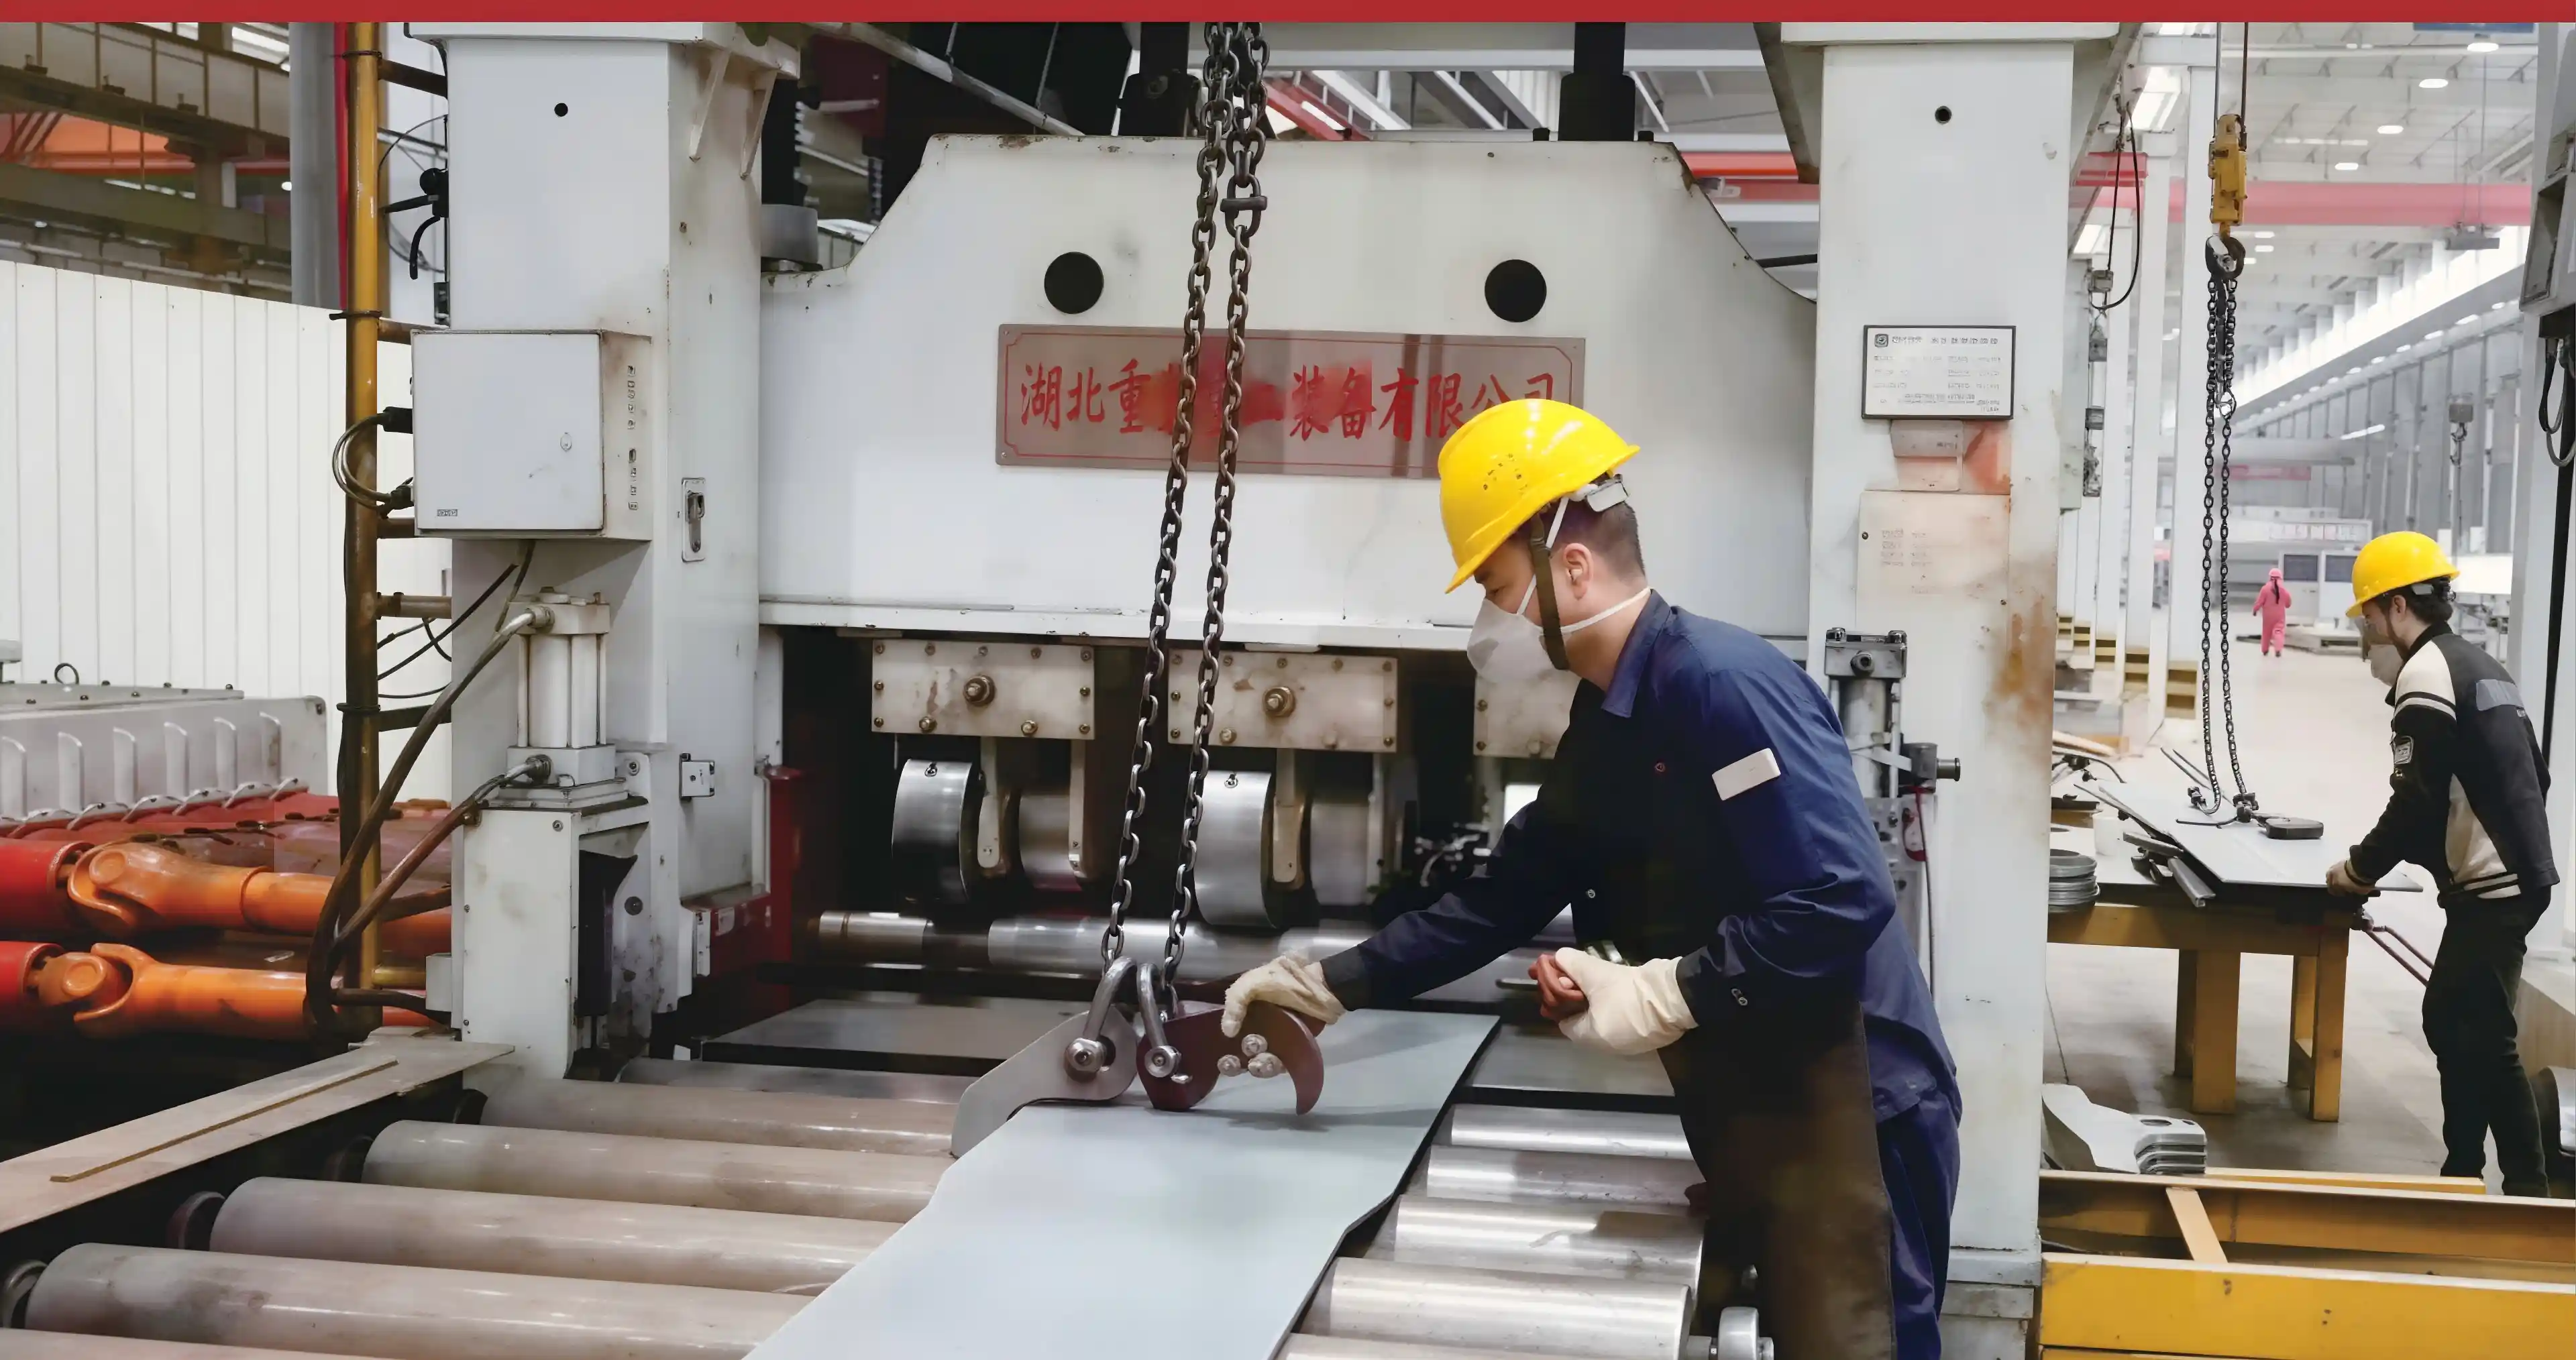
Q355 stress-relieved steel, closed-box construction. Deflection <0.3mm full load vs. 0.8mm standard equipment. Spring isolators reduce vibration 70%. Compact design optimized for thin plate processing.
15 independent SAI hydraulic motors (30-45 kW each). Individual planetary reducers ratio 1:80 per motor. Flow divider maintains ±2% load balance. 4-row backup roller matrix, individually adjustable.
Siemens S7-1200 advanced control module. 4 independent pressure transducers. 15 independent proportional spool valves. <100ms closed-loop adjustment. Stability ±3 bar maintained.
Industrial-grade Siemens PLC. 12-inch advanced operator interface. Absolute position feedback ±0.05mm accuracy. 6 emergency stops, dual-hand enable.
| Model | Max Thickness (mm) | Width (mm) | Yield (MPa) | Rollers | Precision (mm/m²) | Power (kW) | Dimensions |
|---|---|---|---|---|---|---|---|
| EZW43H-8×2000 | 8 | 2000 | 1100 | 15 | 0.5 | 450 | 5600×2400×2600 |
| EZW43H-12×2500 | 12 | 2500 | 1100 | 15 | 0.5 | 550 | 6200×2800×2700 |
| EZW43H-16×3000 | 16 | 3000 | 960 | 15 | 0.5 | 650 | 6800×3100×2900 |
| EZW43H-20×3000 | 20 | 3000 | 960 | 15 | 0.5 | 750 | 7100×3100×3000 |
Material: Q345, advanced high-strength steel; Thickness: 8-16mm; Application: chassis reinforcement, structural panels. Requirement: ±0.5mm flatness, no surface defects.
Material: 690-960MPa high-strength steel; Thickness: 3-12mm; Application: structural support frames. Requirement: perfect flatness, cosmetic finish preservation.
Material: Aluminum alloys, specialty steels; Thickness: 5-20mm; Application: fuselage sections, reinforcement rings. Requirement: ±0.3mm precision, high repeatability.
Material: Stainless 304/316L; Thickness: 8-16mm; Application: equipment frames, pressure housings. Requirement: FDA compliance, zero surface contamination.
Material: High-strength alloys; Thickness: 10-20mm; Application: precision machine bases, structural elements. Requirement: ultra-high flatness (±0.3-0.5mm), vibration isolation.
Challenge:Chassis reinforcement (12mm Q420) requiring ±0.3mm flatness. Previous equipment achieved ±1.0mm. Scrap rate 15%.
Solution:EZW43H-12×2500 with servo pressure control + ML self-learning.
Result:Flatness improved to ±0.35mm; scrap rate reduced to 0.8%; setup time from 30 min to 8 min; annual savings €420K.
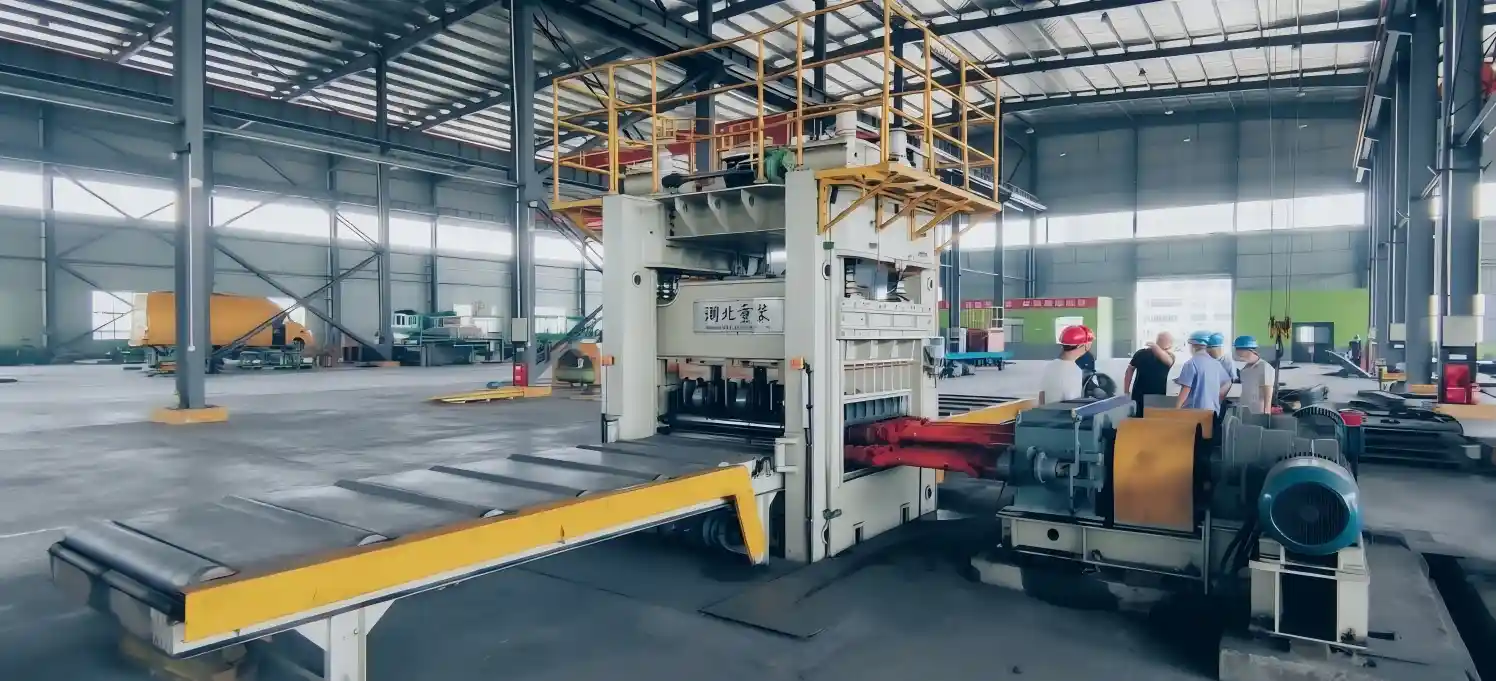
Challenge:Fuselage interior panels (16mm aluminum) requiring ±0.4mm precision. Manual setup inconsistent.
Solution:EZW43H-16×3000 with ML self-learning algorithm.
Result:Precision consistency improved from ±1.2mm variance to ±0.2mm variance; operator training from 3 weeks to 3 days; production efficiency +35%.
All 15 working rollers actively motor-driven. Traditional equipment typically has 3-5 active primary rollers + passive contact rollers. Full drive eliminates passive slip, improving precision to ±0.5mm vs. ±1.0-1.5mm standard.
Operator manually sets parameters for first piece. System learns pressure curve and stores it. Subsequent pieces processed automatically with predicted parameters. New material commissioning reduced 60%.
Full-load minimum radius: 200mm for thin-plate specialty. At half-load: 100mm achievable. 15-roller distributed-force configuration enables tighter radii than traditional equipment.
Optional configuration enables up to 150°C processing. Requires enhanced cooling + thermal insulation. Reduces required pressure 30%, extends equipment life under high-stress applications.
| Item | Lead | Function | Value |
|---|---|---|---|
| Warm-Rolling Package | 10 weeks | 150°C operation capability | 30% pressure reduction, alloy flexibility |
| Advanced SPC Software | 5 weeks | Quality tracking, control charts | Full traceability for regulated industries |
| In-Line Flatness Measurement | 10 weeks | Real-time feedback, auto-correction | ±0.2mm accuracy, zero manual checking |
| Remote Diagnostics | 6 weeks | Cloud monitoring, predictive maintenance | 85% failure prediction accuracy |
| ML Database Expansion | 4 weeks | 50+ new material profiles | Reduces commissioning 60% per new material |