When your shop needs to roll 20mm plate into precision cylinders daily, machine selection impacts material costs, labor hours, and part quality for years. The pre-bending step alone can add 15-20% to cycle time on 3-roll machines, while 4-roll configurations eliminate this entirely—but at what cost?
This comparison breaks down pre-bending efficiency, material waste, operator requirements, and total cost of ownership to help you match machine type to your actual production demands.
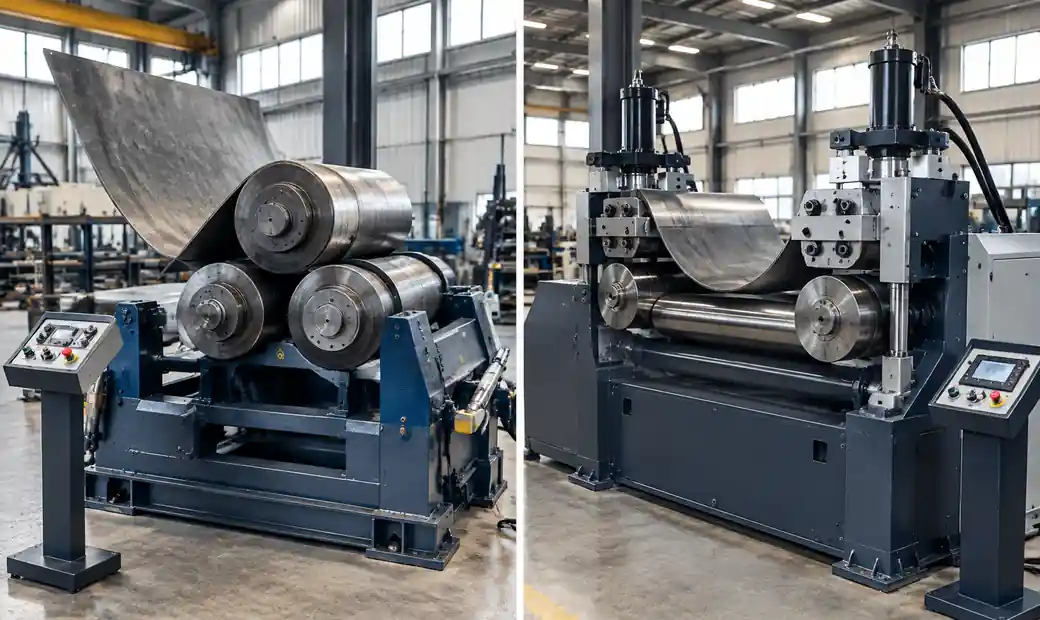 3-roll and 4-roll plate bending machines in workshop setting
3-roll machines use a pyramid configuration: two powered bottom rolls support the plate while a hydraulic top roll applies bending force. You manually pre-bend both plate edges by repositioning the workpiece before rolling the cylinder body.
4-roll machines add a fourth roll that creates a clamping action. The plate feeds between the top and bottom rolls while two side rolls apply symmetrical bending force. This configuration pre-bends edges automatically during the rolling process.
Both achieve cylindrical shells, but the mechanical difference changes how you work.
3-Roll Limitations:
Pre-bending on 3-roll machines requires the operator to flip the plate, reposition it under the rolls, and make 2-4 passes per edge. For a 3m × 12mm plate, expect 8-12 minutes just for edge prep before you start rolling the cylinder.
Straight edge length depends on material thickness and top roll diameter. With 8-12mm plate, you'll leave 1.5× to 2.5× the plate thickness unbent—scrap that needs secondary forming or welding fillout.
4-Roll Advantage:
The clamping configuration eliminates manual pre-bending. Edge bending happens automatically as the side rolls apply force during the first pass. The same 3m plate now takes 3-5 minutes from start to finished cylinder.
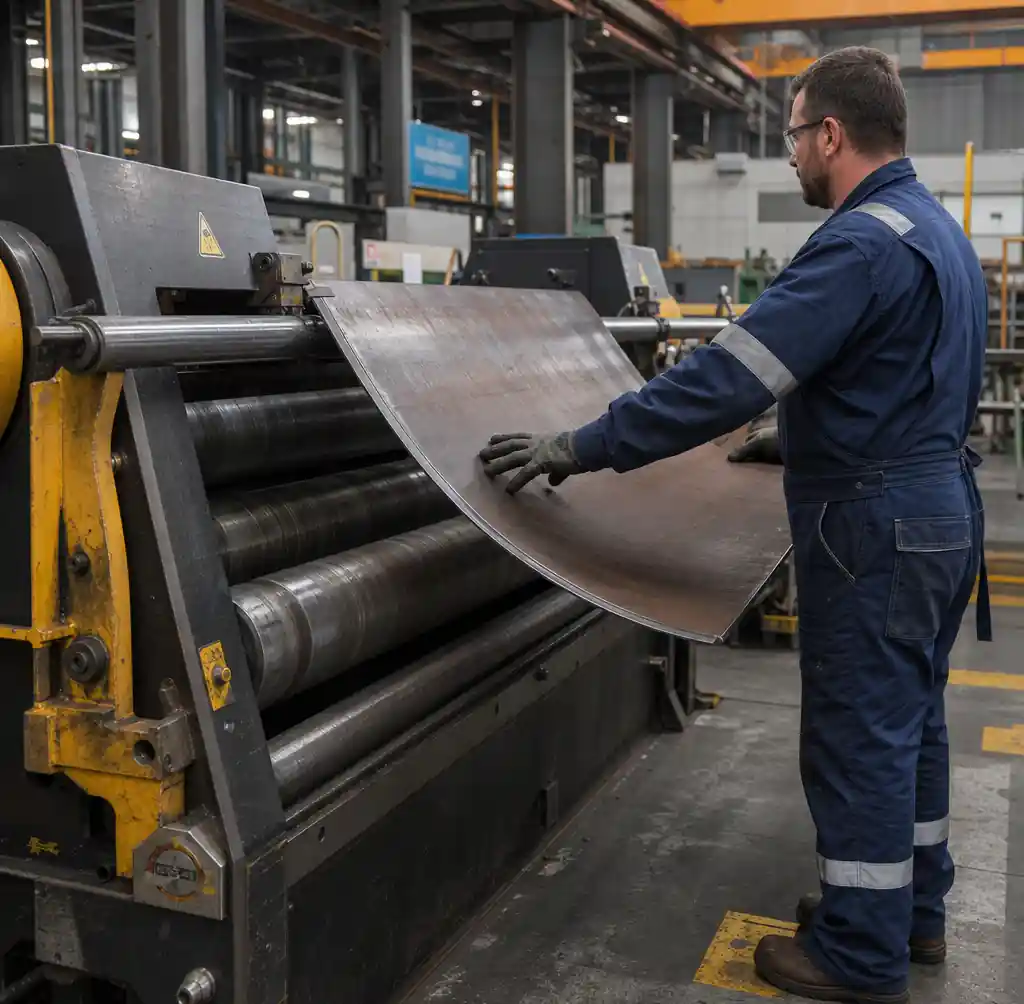 Operator performing manual pre-bending on 3-roll machine
Residual straight edge drops to 0.5× plate thickness or less. On 12mm plate, you reduce waste from 30-36mm per edge to 6-8mm—material savings that compound across hundreds of shells.
| Pre-Bending Factor | 3-Roll | 4-Roll |
|---|---|---|
| Manual Pre-Bending Required | Yes, 8-12 min per plate | Automatic, integrated |
| Straight Edge Waste | 1.5-2.5× thickness | 0.5× thickness or less |
| Operator Skill Level | Intermediate to advanced | Entry to intermediate |
| Setup Time (typical shell) | 15-20 minutes | 5-8 minutes |
On 3-roll machines, those unbent edges become scrap or require secondary operations. For a pressure vessel project using 50 plates at 12mm × 3m, you're looking at 90-180mm of waste per plate—4.5 to 9 meters of 12mm material across the job.
At $800-1,200 per ton for steel plate, waste adds up. A shop rolling 100 shells per month could lose $15,000-25,000 annually just to straight edges that need rework.
4-roll machines reduce this waste by 60-75%. The same vessel project now wastes 1.8-3.6 meters instead of 9. Over a year, material savings alone can offset 15-20% of the 4-roll machine's price premium.
3-Roll Machines:
Experienced operators learn to "feel" the right pressure and positioning for pre-bending. New operators need 3-6 months to consistently produce cylinders within ±2mm diameter tolerance. Edge quality varies between operators, and turnover means retraining costs.
The 3-roll S-type reduces some skill dependency with adjustable lower rolls, but pre-bending remains manual.
4-Roll Machines:
CNC controls eliminate guesswork. Operators input diameter, thickness, and material—the machine calculates roll positions. Entry-level operators produce consistent results within 2-3 weeks. Less tribal knowledge means lower training costs and faster production ramp-up.
Purchase price tells half the story. A 3-roll machine with 30mm × 3000mm capacity runs $45,000-75,000. The equivalent 4-roll configuration costs $85,000-140,000—roughly 60-90% more upfront.
But total cost includes:
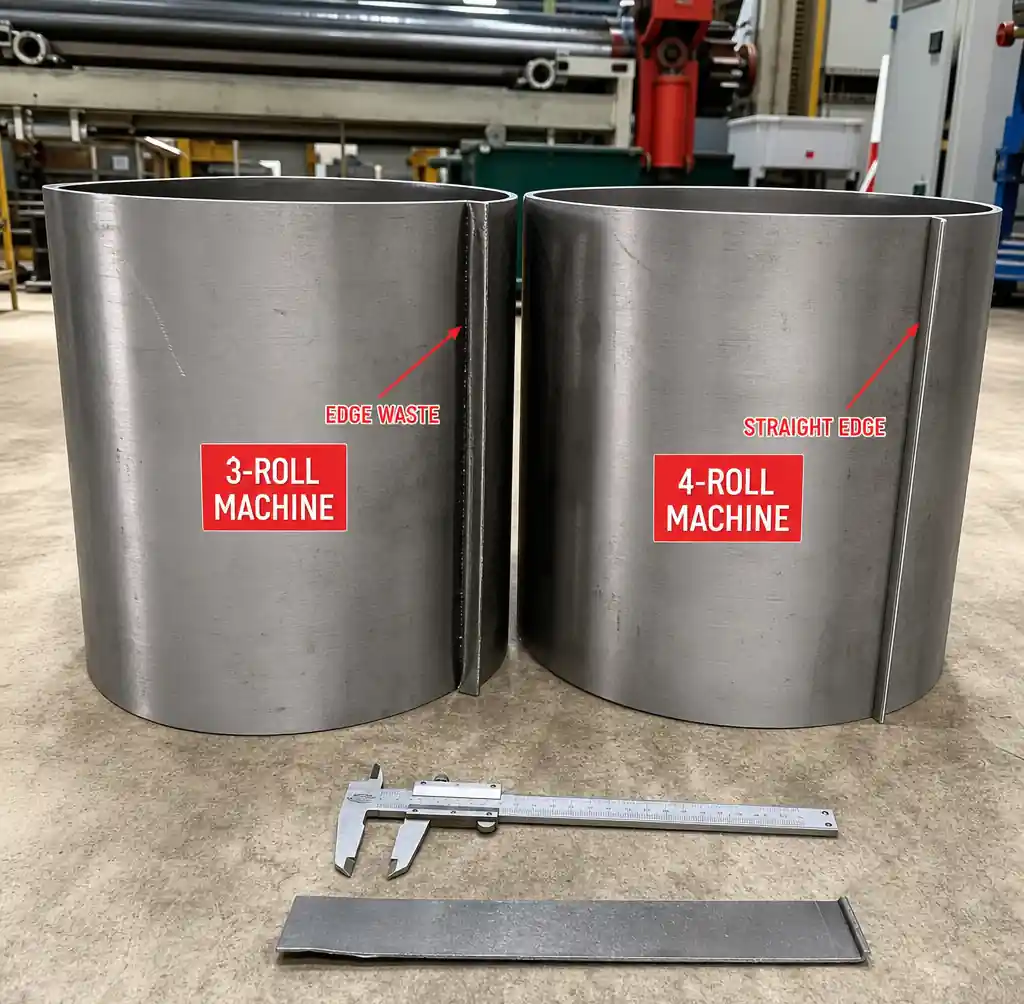 Rolled cylindrical shells showing edge quality comparison
A shop running two shifts and rolling 120-150 shells monthly typically sees payback on the 4-roll premium within 24-36 months from material and labor savings alone.
| Cost Factor (Annual) | 3-Roll Shop | 4-Roll Shop | Difference |
|---|---|---|---|
| Machine Price (amortized 10yr) | $6,000-7,500 | $11,000-14,000 | +$5,000-6,500 |
| Material Waste | $18,000-25,000 | $4,500-7,500 | -$13,500-17,500 |
| Labor Hours (150 shells/mo) | 450 hr | 270 hr | -180 hr |
| Labor Cost (@$35/hr) | $15,750 | $9,450 | -$6,300 |
| Net Annual Difference | — | — | -$14,800-17,300 savings |
Choose 3-Roll When:
Choose 4-Roll When:
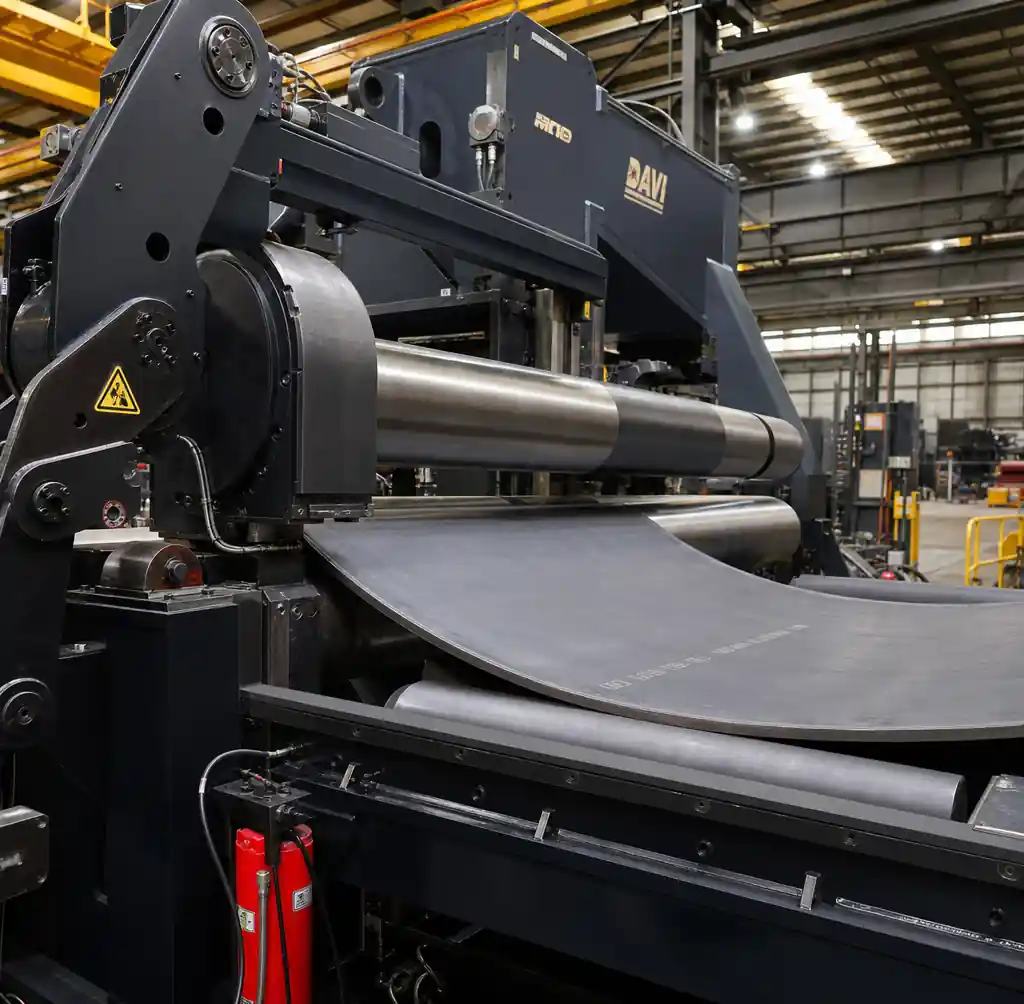 Heavy plate rolling operation on 4-roll machine
Most selection guides focus on technical specs. Real-world shops need to calculate based on actual production:
Monthly Shell Count: Count your rolling jobs over 90 days. Include everything from small tank ends to large cylinders. If you're over 40-50 shells monthly, 4-roll economics shift strongly favorable.
Average Plate Thickness: Shops working predominantly 12mm and under can often justify 3-roll. Once you're regularly rolling 16-25mm plate, the pre-bending labor penalty becomes prohibitive.
Material Costs: Calculate your annual plate purchases. If you're spending $300,000+ per year on steel, the 4-roll waste reduction pays for itself quickly.
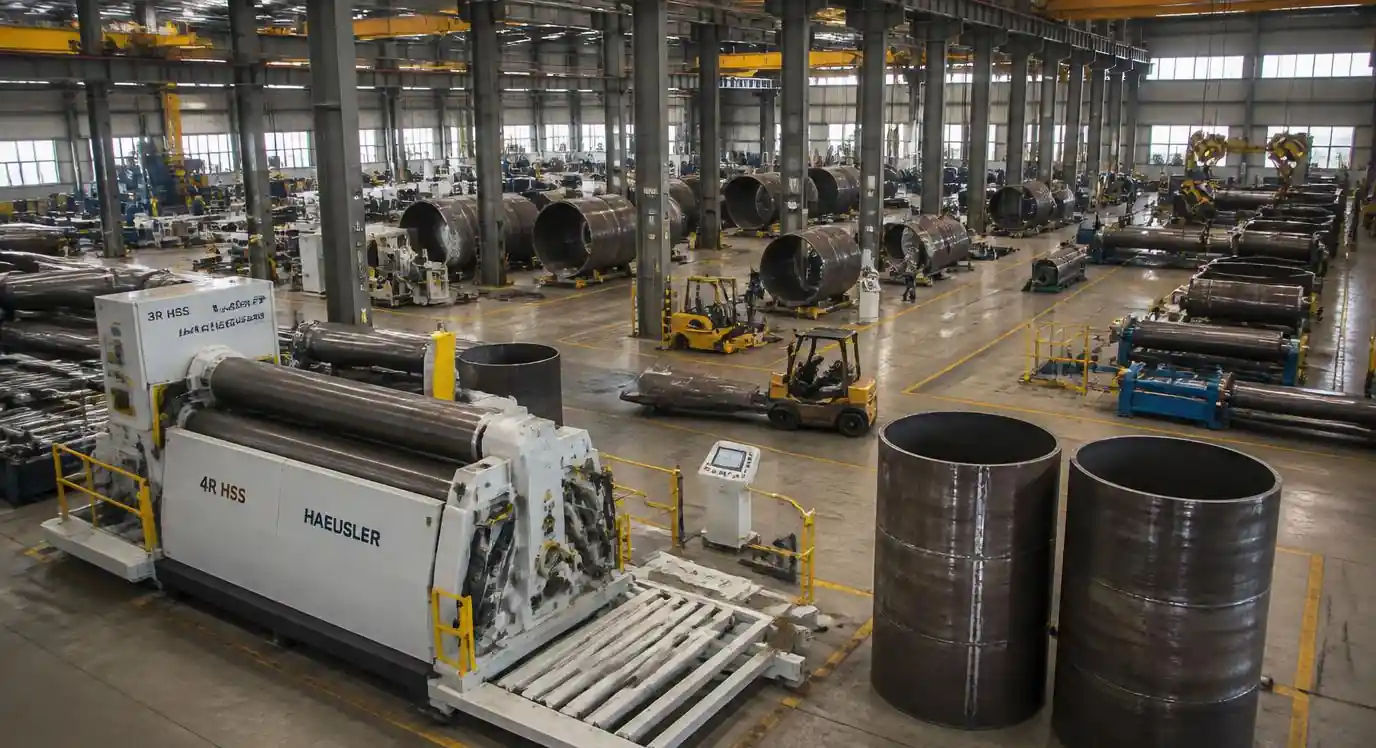 Fabrication shop with multiple plate rolling machines
Labor Availability: In regions with skilled metal workers, 3-roll remains viable. Where labor is tight or turnover high, 4-roll's lower skill requirement protects production capacity.
| Workshop Profile | Monthly Volume | Plate Thickness | Material Spend | Recommended Choice |
|---|---|---|---|---|
| Small Job Shop | 15-30 shells | 6-16mm | $50K-150K/yr | 3-Roll + skilled operator |
| Mid-Size Fabricator | 40-80 shells | 10-25mm | $200K-400K/yr | 4-Roll (24-36mo payback) |
| Pressure Vessel Shop | 50-100 vessels | 16-40mm | $400K-800K/yr | 4-Roll (18-24mo payback) |
| Wind Tower Manufacturer | 80-150 sections | 20-60mm | $800K+/yr | 4-Roll CNC (12-18mo payback) |
Can a 4-roll machine do everything a 3-roll does?
Yes, for cylindrical work. 4-roll machines handle cylinders, pipes, and straight rolling. However, 3-roll configurations offer easier setup for frequent cone rolling due to the pyramid geometry. If you roll cones more than 20% of the time, consider this trade-off.
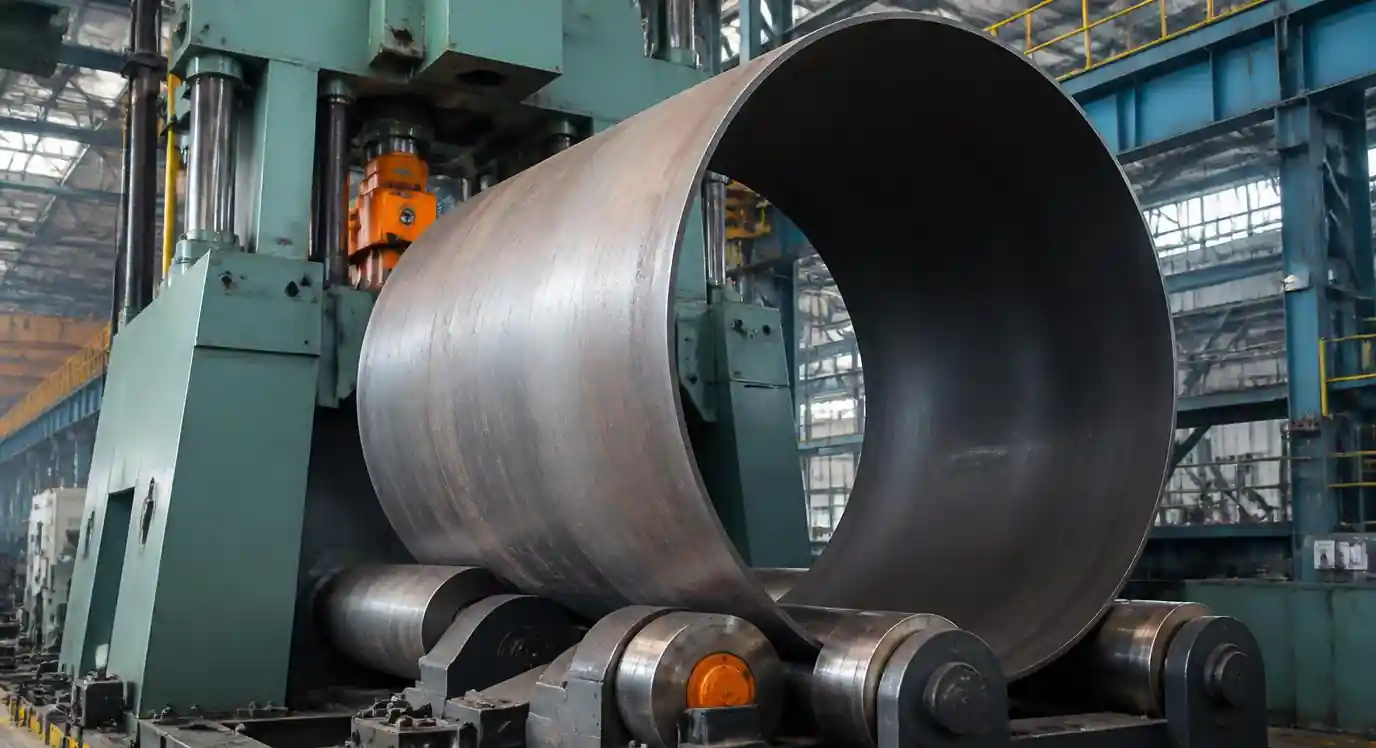 Pressure vessel shell being formed on plate rolling machine
How much does operator experience matter with each type?
On 3-roll machines, operator skill directly affects quality. Expect 3-6 months for new operators to reach full proficiency. On 4-roll CNC systems, operators produce consistent parts within 2-3 weeks. Shops with high turnover see significant productivity protection with 4-roll.
What about maintenance costs?
3-roll machines have fewer hydraulic components and simpler mechanical systems, typically costing $2,000-4,000 annually for maintenance. 4-roll machines with CNC add servo systems and more hydraulic cylinders, running $4,000-7,000 per year. The difference is real but small compared to operational savings.
Can I upgrade from 3-roll to 4-roll later?
No. The frame geometry and roll configuration are completely different. This is a one-time choice. However, you can start with 3-roll and add a 4-roll machine later as volume grows, running both for different applications.
Which gives better diameter accuracy?
4-roll machines deliver tighter tolerances due to continuous clamping force and symmetrical bending. Expect ±1-1.5mm diameter accuracy on 4-roll CNC systems versus ±2-3mm on 3-roll with skilled operators. For pressure vessel work requiring ASME Section VIII compliance, 4-roll reduces rework.
What thickness range is the "tipping point" for 4-roll?
Most shops find the payback justification clear when regularly rolling 16mm and thicker. Below 12mm, 3-roll remains competitive unless volume is very high (100+ shells/month). The 12-16mm range is where operational analysis determines the right choice.
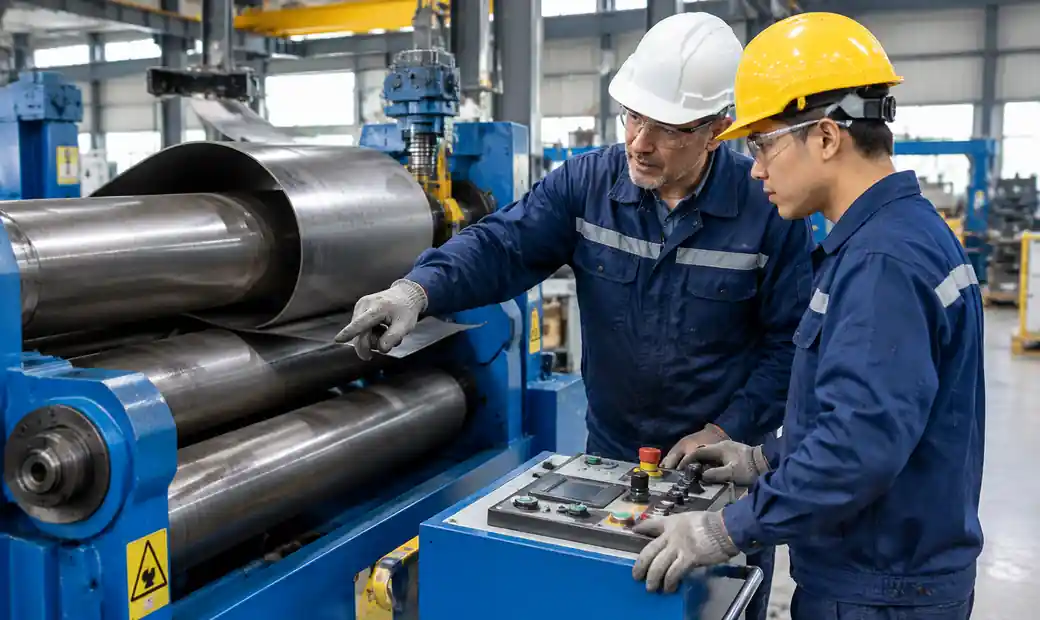 New operator learning plate rolling machine operation
The 3-roll versus 4-roll decision comes down to production volume, plate thickness, and total cost analysis rather than machine capability alone. 3-roll machines remain cost-effective for shops rolling fewer than 40 shells monthly with thinner materials and experienced operators. The lower purchase price and simpler maintenance fit job shop economics.
4-roll machines deliver measurable ROI for mid-to-high volume fabricators through 40-55% faster cycle times, 60-75% less material waste, and lower operator skill requirements. Shops processing 50+ shells monthly or working with 16mm+ plate typically achieve payback within 24-36 months from operational savings alone.
Calculate your actual monthly shell count, average material thickness, and annual plate costs. Run the numbers against the cost table above—the right choice becomes clear based on your specific production reality rather than general capability comparisons.
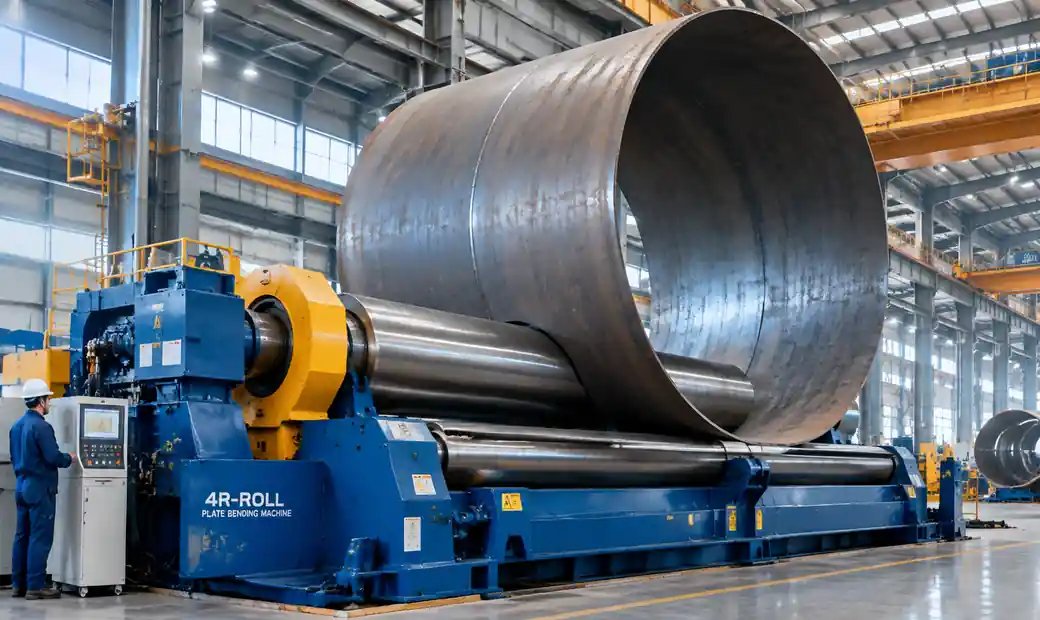 Wind tower section being rolled on heavy-duty machine
EZHONG manufactures both 3-roll and 4-roll plate rolling machines from 6mm to 200mm × 6000mm capacity, serving fabricators in pressure vessel, wind tower, tank, and pipe manufacturing worldwide. Contact our technical team for capacity analysis and machine recommendations based on your production requirements.